Engineered Nonwoven Formulations for Uzbekistan Industrial Demands
Direct supply lines engineered for high dimensional stability, cross-directional tensile equilibrium, and medical-grade purity.
-
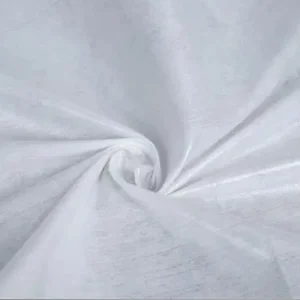
Uzbekistan High-Tensile Parallel Spunlace Nonwoven Fabric
Explore Technical Specs -
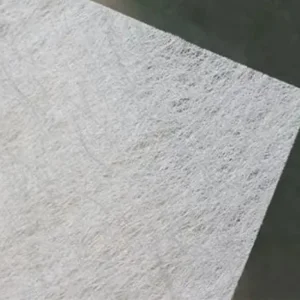
Filament Spunbond Nonwoven Fabric for Central Asian Engineering
Explore Technical Specs -
Semi-Cross Lapped Spunlace Nonwoven for Regional Converters
Explore Technical Specs -
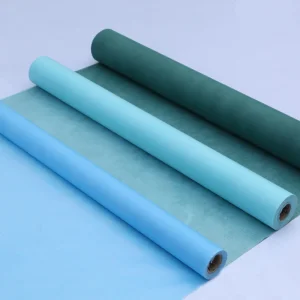
Precision Chemical Bond Nonwoven Fabrics for Industrial Linings
Explore Technical Specs
Macro Industrial Transformation of Uzbekistan's Manufacturing Ecosystem
From primary agrarian cotton processing to an advanced regional technical textiles and nonwoven material powerhouse.
The Republic of Uzbekistan is currently experiencing one of the most consequential economic reconfigurations in Central Asia. Driven by the comprehensive national objectives codified under the Strategy Uzbekistan 2030, the country has systematically transitioned away from the export of raw natural resources toward vertically integrated, high-value-added advanced processing. Central to this strategic industrial pivot is the modernization of the industrial manufacturing process: moving downstream from basic carded cotton lint toward high-tech polymer extrusion, mechanical water-jet hydroentanglement, chemical bonding, and specialty composite finishing.
Historically recognized as a global agricultural epicenter for raw cotton fibers, Uzbekistan has ended raw lint shipments to establish domestic cotton-textile clusters spanning Tashkent, Fergana, Andijan, Samarkand, and Navoi. However, the rapid acceleration of secondary processing across the automotive (UzAuto OEM ecosystems in Asaka), filtration, building construction, and healthcare markets has exposed an urgent need for technically reliable nonwoven substrates. Traditional textiles cannot satisfy the tight mechanical tolerances, biological safety profiles, and chemical resistance thresholds demanded by modern industrial buyers. The manufacturing paradigm has shifted toward state-of-the-art nonwoven processing lines that offer precise control over Machine Direction (MD) and Cross Direction (CD) tensile ratios, isotropic fiber distributions, and chemically inert bonding matrices.
The Role of Free Economic Zones (FEZ) in Driving Substrate Demand
Within high-growth hubs such as the Navoi Free Industrial Zone (FIEZ), Angren FEZ, and Jizzakh Special Economic Zone, enterprise converters are integrating nonwoven media into multi-layer laminates, construction membranes, and synthetic leather backing cloth. For engineering and procurement leaders operating in these zones, the primary bottleneck has historically been localized consistency: variation in fiber web grammage (GSM), poor bonding cohesion, and inconsistent surfactant washes. A technically robust production process manufacturer eliminates these defects by integrating closed-loop automated optical scanning, precision opening rollers, and dynamic web cross-lapping into the manufacturing line.
Systemic Industrial Upgrading
By blending indigenous raw fibers (refined cotton, bio-viscose) with advanced synthetic polymer inputs (Polyester PET, Polypropylene PP, Polylactic Acid PLA), modern processing manufacturers enable Uzbekistan converters to compete directly with European Union and East Asian supply chains under the EU Generalized Scheme of Preferences Plus (GSP+) regulatory umbrella.
Precision Engineering of the Nonwoven Production Process
A rigorous examination of hydroentanglement mechanics, multi-stage carding, and functional chemical consolidation.
Fiber Opening & Micro-Blending
The manufacturing process begins with pneumatic bale opening and high-precision gravimetric blending. staple fibers—such as ultra-pure polyester, functionalized polypropylene, and regenerated cellulose—are opened through coarse and fine pinned rollers. This eliminates dense fiber bundles, ensuring isotropic distribution across the cross-sectional web plane and preventing localized grammage deviations.
Multi-Stage Carding & Lapping
Carding cylinders operating with micro-calibrated wire cloth transfer individual fibers into a coherent parallel web. Depending on target physical characteristics, the process utilizes high-speed parallel carding for longitudinal strength or precision cross-lappers with variable profile profiling systems. This balances MD/CD tensile ratios and eliminates edge-to-center thickness variations.
High-Pressure Hydroentanglement
The core spunlace process forces micro-fine water jets—pressurized from 30 to over 250 bar through platinum-iridium or stainless steel nozzle strips (orifice diameters: 0.08–0.12 mm)—into the continuous fiber web. This mechanical entanglement twists and interlocks staple fibers around one another without thermal melt degradation or chemical binders, producing high softness and tensile integrity.
| Process Parameter | Parallel Spunlace Route | Full-Cross Lapped Spunlace | Chemical Bond Nonwoven | Filament Spunbond Polymeric |
|---|---|---|---|---|
| Target Tensile Ratio (MD:CD) | 3.5 : 1 – 5.0 : 1 | 1.0 : 1 – 1.3 : 1 (Isotropic) | 2.0 : 1 – 3.2 : 1 | 1.2 : 1 – 1.5 : 1 |
| Grammage Versatility (GSM) | 30 gsm – 80 gsm | 40 gsm – 250 gsm | 20 gsm – 120 gsm | 15 gsm – 180 gsm |
| Fiber Component Selection | Viscose / PET Blends | PET, Viscose, PLA, Cotton | PES, Regenerated Fiber | Virgin Polypropylene (PP), PET |
| Binder Chemistry Application | Zero Binder (Pure Hydraulic) | Zero Binder (Pure Hydraulic) | Acrylic, EVA, Nitrile Emulsions | Thermal Calender Consolidation |
| Primary Mechanical Characteristic | High longitudinal line speed | Equal biaxial strength, low drape shear | High stiffness, dimensional recovery | Continuous filament tear resistance |
Localized Application Scenarios Across Uzbekistan's Industrial Nodes
Purpose-engineered nonwoven media integrated across key regional economic sectors.
Automotive OEM Components (Asaka & Samarkand)
Supplying Tier-1 and Tier-2 manufacturers supporting the UzAuto Motors supply chain. Hydroentangled cross-lapped substrates serve as acoustic deadening matrices, interior headliner backing fabrics, and primary carpet backing. Nonwovens must withstand deep-draw thermoforming without localized necking, while meeting strict European VOC and fogging limitations (DIN 75201 standards).
Mining, Heavy Industry & Metallurgy (Navoi & Almalyk)
Navoi Mining & Metallurgical Combinat (NMMC) and Almalyk Mining and Metallurgical Complex (AMMC) require industrial air pollution control and high-temperature filtration. In these aggressive environments, advanced needle-punched and spunlace basalt, PTFE, and polyimide (PI) media operate at temperatures exceeding 240°C, resisting acid gas hydrolysis and capturing particulate matter down to sub-micron scales.
Agricultural Micro-Climate Management (Fergana & Surkhandarya)
The agricultural valleys of eastern and southern Uzbekistan face volatile seasonal microclimates, including sharp spring frosts and extreme arid heat. UV-stabilized polypropylene filament spunbond and chemically bonded agrolayers provide micro-porous crop coverings. These permeable barriers preserve soil moisture, modulate evapotranspiration rates, and shield crops from windborne desert dust without trapping heat.
Healthcare & Hygiene Disposables (Tashkent Industrial Hub)
Modern cleanrooms within Tashkent's pharmaceutical corridor convert pure spunlace nonwovens into lint-free surgical gowns, surgical drape laminates, and single-use hygienic wipe systems. Utilizing medical hydroentanglement with closed-circuit filtration delivers low bio-burden counts, hypoallergenic skin contact, and chemical compatibility with alcohol disinfectants.
Localized Support, Compliance Guarantees, & Technological Roadmap
Aligning international engineering specifications with Uzbek state standards (O'zDSt) and global regulatory bodies.
Quality Assurance & Regulatory Alignment
For international manufacturers supplying downstream partners across Uzbekistan, compliance cannot be an afterthought. Production lines must meet ISO 9001:2015 quality frameworks and ISO 13485 medical device criteria, while complying with local Technical Regulations (O'zTR) and sanitary-epidemiological safety standards. Our production processes enforce lot-to-lot traceability from incoming fiber polymer certification to outgoing slitted roll profiles.
- Standardized testing for tensile breaking force (ISO 9073-3) and hydrohead pressure.
- OEKO-TEX Standard 100 Class I verification for direct-to-skin medical & baby hygiene.
- Consistent air permeability, pore sizing, and bubble point testing for filtration media.
Phase I: Advanced Closed-Loop Hydro-Recovery (Present)
Deployment of multi-stage dissolved air flotation (DAF) and sand-membrane water filtration systems across hydroentanglement processing lines. Reclaims 96% of process water, minimizing environmental footprints in Central Asia's arid regions.
Phase II: Integration of Pure Bio-Polymer Extrusion (2025–2027)
Transitioning petroleum-derived polyester and polypropylene inputs to Polylactic Acid (PLA), Polyhydroxyalkanoates (PHA), and high-tenacity regenerated cellulose. Enables 100% industrially compostable nonwovens for agricultural and single-use hygiene markets.
Phase III: AI-Driven Optical Inspection & Closed-Loop Calendering (2028+)
Implementing inline high-speed machine vision systems paired with machine learning algorithms. Scans 100% of the moving web at up to 600 m/min, detecting micro-contaminants, web thin spots, and pinholes, with automated, real-time adjustments to hydraulic jet pressures.
High-Performance Nonwoven Lines Engineered for Converting Operations
Specialty fibers, functional surfaces, and custom-calendered web structures for industrial, medical, and filtration operations.
-
Full-Cross Spunlace Nonwoven Fabric for Engineering Layers
Explore Technical Specs -
High-Temperature Basalt Nonwoven Fabric for Thermal Barriers
Explore Technical Specs -
Carbon Fiber Nonwoven Web for Lightweight Composite Formulations
Explore Technical Specs -
Medical-Grade Plain Spunlace Nonwoven for Converting Mills
Explore Technical Specs -
Filament Spunbond Substrate for Agricultural Infrastructure
Explore Technical Specs -
Chemically Resistant PTFE Nonwoven Fabric for Corrosive Filtration
Explore Technical Specs -
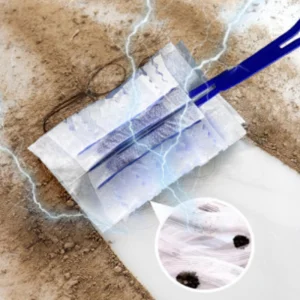
Electrostatic Adsorption Spunlace Fabric for Particulate Capture
Explore Technical Specs -
High-Elastic Spunlace Nonwoven Fabric for Ergonomic Bandaging
Explore Technical Specs
Frequently Asked Technical & Sourcing Inquiries
Addressing engineering specifications, logistical handling, and material compatibility for the Central Asian market.
The difference lies in fiber orientation mechanics. Parallel-laid spunlace is formed with fibers oriented predominantly in the longitudinal machine direction (MD). This yields high processing speeds and high MD tensile strength, but lower cross-direction (CD) resistance, making it ideal for wipes and hygiene conversions. Cross-lapped spunlace folds carded webs diagonally across the conveyor, yielding isotropic 1:1 to 1:1.3 MD:CD ratios. This prevents necking or deformation during coating, PU synthetic leather lamination, and automotive structural molding.
For clinical barrier performance, we recommend a 55% woodpulp / 45% polyester (PET) or a 70% viscose / 30% polyester composite, typically in 50 to 68 GSM specifications. Hydroentangled webs can be treated with topical fluorochemical finishes to achieve repellent ratings against blood, bodily fluids, and alcohol penetration (level 3 and level 4 barrier standards per AAMI PB70 and EN 13795).
For agricultural and construction installations in regions like Tashkent, Bukhara, and Navoi, synthetic polymers are blended with Hindered Amine Light Stabilizers (HALS) and anti-UV concentrates. This prevents ultraviolet photo-degradation, polymer chain scission, and brittleness under intense solar irradiation, maintaining tensile properties over multi-season deployments.
Every master production roll undergoes inline optical defect scanning for pinholes and foreign matter, followed by laboratory validation. Standard QA checks measure grammage consistency (ISO 9073-1), thickness under specified pressure foot gauges (ISO 9073-2), strip tensile break-force and elongation (ISO 9073-3), water absorbency time/capacity (ISO 9073-6), and hydrostatic liquid head resistance (AATCC 127).
Yes. In addition to primary hydroentanglement and bonding, our production ecosystem includes multi-functional padding, foulard dyeing, rotary screen printing, and chemical sizing equipment. We can supply water-repellent, anti-static, antimicrobial, hydrophilic, and flame-retardant (compliant with FMVSS 302 and DIN 4102 B1) modifications customized to your specification sheet.
Optimize Your Nonwoven Production Pipeline Today
Connect with our engineering specialists to specify fiber blends, mechanical tensile profiles, and functional finishes tailored to your manufacturing requirements in Uzbekistan and the broader Central Asian region.
Send Inquiry Now