Primary Technical Portfolio
Standard & Functional Spunlace Solutions
Explore eight core solutions engineered directly within our continuous hydroentanglement lines, serving cross-industry converting specifications.
High-Quality Filament Spunbond Nonwoven Fabric Products Supplier, Factories
View Specifications
High-Quality Semi-Cross Lapped Spunlace Nonwoven Fabric Products Factories, Product
View Specifications
High-Quality Chemical Bond Nonwoven Fabrics Manufacturer, Company
View Specifications
High-Quality Full-Cross Spunlace Nonwoven Fabric Products Factories, Companies
View Specifications
China Black Viscose Spunlace Nonwoven Fabric Products Suppliers, Factory
View Specifications
High-Quality Aramid Nonwoven Fabrics Manufacturers, Companies
View Specifications
China Far-Infrared Negative Lon Nonwoven Fabric Products Suppliers, Factory
View Specifications
Engineering Deep Dive
Industrial Production Process in Modern Manufacturing Factories
A granular perspective on how integrated smart factory ecosystems orchestrate raw polymers, fiber opening, hydroentanglement, and closed-loop wet finishing.
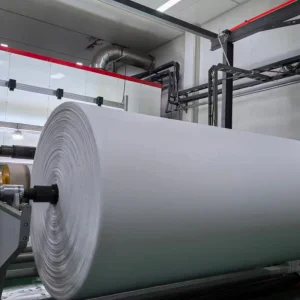
In modern nonwoven textile manufacturing, the distinction between standard conversion mills and tier-one production process factories lies within their precision web-forming and high-pressure water-needle hydroentanglement controls. Operating out of Changshu, Jiangsu Province, YDL Nonwovens (Changshu Yongdeli Spunlaced Non-woven Fabric Co., Ltd.) has continually engineered state-of-the-art spunlace technologies since 2007. The core factory paradigm transitions beyond basic assembly: it manages mechanical carding kinetics, high-pressure continuous fluid dynamics, thermodynamic moisture management, and in-line chemical grafting under one continuous, automated infrastructure.
Fiber Opening, Dynamic Blending, and Multi-Stage Carding Kinetics
The production lifecycle begins with raw staple fiber selection. Industrial processes manage specialized compositions across virgin Polyester (PET), regenerated Viscose/Rayon, Polypropylene (PP), biodegradable Polylactide (PLA), as well as extreme-performance inorganic filaments such as Aramid, Pre-oxygenated fibers, Basalt, and Polyimide. Bale plucking machines deploy micro-load pneumatic sensors to feed balanced fiber blends into fine-opener cylinders. This mechanical action individualizes fibers without damaging their structural crimp, ensuring high volumetric bulking.
Subsequently, high-speed carding engines arrange random fiber matrices into targeted web designs. A critical distinction in our production lines is the capability to alternate between Parallel Carding (yielding high Machine Direction tensile strength suited for wipes and hygiene goods) and Cross-Lapped / Semi-Cross Lapped Webs (which equilibrate the MD/CD tensile ratio to approximately 1:1). This mechanical manipulation eliminates transverse stretch fatigue, making cross-lapped substrates the global standard for synthetic leather backing and industrial filtration media.
High-Pressure Hydroentanglement Dynamics: Water-Needle Precision
At the core of the spunlace factory floor sits the multi-stage hydroentanglement manifold. Unbonded fiber batts pass over perforated nickel suction cylinders or structural patterning drums while being subjected to progressive rows of high-pressure micro-water jets (operating at pressures ranging from 30 bar up to 250 bar). The kinetic energy delivered by these micro-jets forces the fibers to twist, rotate, and entangle around adjacent fibers. Because no chemical binders, thermal resin lattices, or synthetic starches are applied during web consolidation, the resulting fabric preserves its inherent fiber softness, ultra-low lint profile, and superior drapeability.
The engineering triumph of this phase relies on real-time deionization and closed-loop water treatment. Water circulating through our hydraulic jets is continuously filtered through multi-media sand filters, active carbon filters, and micro-porous bag systems. By monitoring total dissolved solids (TDS) and continuous surface tension, jet orifice clogging is mitigated, ensuring consistent physical aperture geometries across master rolls exceeding 3.2 meters in working width.
| Process Stage | Core Mechanism | Target Output Metrics | Industrial Application Focus |
|---|---|---|---|
| Fiber Blending | Automated micro-weighing & pneumatic opening | Uniform fiber dispersion (PET/Viscose/PLA) | Hygiene, Medical disposables, Premium wipes |
| Cross-Lapping | Reciprocating carriage web laying | Balanced MD:CD tensile strength (approaching 1:1) | Automotive PU synthetic leather substrates |
| Hydroentanglement | Multi-stage pressurized water injectors (30–250 bar) | Binder-free consolidation, high burst strength | Surgical gowns, Micro-apertured cosmetic masks |
| Wet-Chemical Finishing | Pad-dry-cure, immersion bath & foam coating | Water repellent, Flame retart, Thermochromic | Thermal fire barriers, Military garments, HVAC filters |
| In-Line Inspection | Optical CCD camera scanners & beta gauges | Zero defect roll tagging, GSM uniformity ±1.5% | Cleanroom wipes, High-precision membrane supports |
Macro Industry Ecosystems
End-to-End Enterprise Solutions Across Sectors
Addressing structural supply chain vulnerabilities through integrated chemical, thermal, and mechanical conversion under one industrial roof.
Medical & Life Sciences
Certified cleanroom conversion requires absolute biosecurity, biological neutrality, and zero chemical toxicity. Our spunlace production process integrates bio-compatible viscose and hydrophobic polyester blends finished with fluorochemical-free water repellents and anti-microbial coatings. These configurations withstand gamma-ray, ethylene oxide (EtO), and autoclave steam sterilization without degrading fiber bonding, fulfilling stringent criteria for Class II surgical drapes, wound contact dressings, and bacterial fluid barriers.
Automotive & Synthetic Leather
Synthetic PU/PVC leather manufacturers face challenges regarding delamination, stretching, and edge curling during coagulating baths. YDL solves these issues using full-cross spunlace substrates engineered with exact surface smoothness and thermal shrinkage stability under 1%. By coordinating in-house sizing (stiffness adjustments) and reactive offline dyeing, our base fabrics yield flawless polymeric resin adhesion for luxury automotive seating, dashboards, and heavy-duty upholstery.
Advanced Technical Filtration
Industrial gas purification and liquid filtration demand deep-bed media capable of operating under corrosive chemical exposure and extreme temperatures. Utilizing technical precursors including Pre-oxygenated filaments, Basalt fibers, and Polyimide (PI), our factories weave hydroentangled nonwoven felts that maintain particulate trapping efficiencies down to PM2.5, retaining structural integrity above 260°C in coal-fired emissions, metallurgical smelting, and chemical processing plants.
Global Strategy & Local Compliance
Commercial Status, Export Logistics & Regulatory Safeguards
Aligning mass production volume with regional compliance mandates for frictionless worldwide delivery.
ISO 9001:2015 QC Protocols
Every production batch is indexed against documented quality procedures. In-line camera defect detection systems map fiber density variations, pinholes, and foreign bodies, automatically rejecting non-conforming roll yards prior to slitting.
EU REACH & RoHS Compliance
Our functional finishing chemistries—including flame retardants, biocides, and colorants—are independently audited to guarantee zero SVHCs (Substances of Very High Concern), fluorinated PFAS, or hazardous heavy metal catalysts.
Global Multimodal Freight Ready
Master rolls undergo vacuum-compressed shrink wrapping with reinforced multi-layer polyethylene sheeting. Optimized roll diameters minimize empty space in 40ft High Cube containers, preserving core concentricity through intermodal ocean transit.
Regional Technical Support
Our engineering desk collaborates with converter production teams across Europe, North America, Southeast Asia, and the Middle East, fine-tuning slit tolerances, web tensions, and spool winding tensions for high-speed automated packaging machinery.
Horizon 2026–2030
Engineering Roadmap: Digitalization & Circular Polymers
Pioneering sustainable materials, AI-driven process controls, and functional composite surfaces.
Phase I · Optimization
Closed-Loop Hydration Analytics
Implementation of AI-driven hydrodynamic feedback loops that modulate pump motor frequencies to real-time fiber thickness, reducing energy consumption per square meter by 18%.
Phase II · Decarbonization
100% Bio-Circular Feedstocks
Expanding the processing throughput of certified compostable PLA, bamboo viscose, and lyocell fibers to assist consumer packaging conglomerates in ditching single-use fossil-derived plastics.
Phase III · Functionalization
Micro-Encapsulated Active Chemistry
Continuous inline grafting of phase-change materials (PCM), photo-responsive dyes, and anti-mite botanical agents directly inside hydroentanglement drums, preventing chemical wash-out.
Phase IV · Intelligence
Smart Industrial Fabrics
Embedding conductive stainless steel and carbon filaments into high-strength aramid base structures for real-time stress and temperature telemetry in aerospace and structural containment shielding.
Technical Clarity
Frequently Asked Questions on Factory Production
In-depth responses for procurement directors, mechanical engineers, and compliance officers.
What is spunlace nonwoven fabric, and how does the manufacturing process differ from chemical or thermal bonding?
Spunlace (hydroentangled) nonwoven fabric is manufactured by carding loose staple fibers into a uniform fibrous web and subjecting it to high-velocity, high-pressure micro-water jets. Unlike chemical bonding—which utilizes synthetic polymer binders (like acrylic or EVA resins)—or thermal bonding (which melts low-melting-point binder fibers via calender heat), hydroentanglement uses mechanical friction and water kinetic energy to interlock the filaments. The result is an exceptionally soft, breathable, drapable fabric that offers high tensile strength and virtually zero lint, making it pure enough for medical, personal care, and high-performance cleanroom applications.
Which fiber polymers and technical filaments can YDL Nonwovens process across its factory lines?
Our flexible manufacturing lines routinely process conventional organic and synthetic polymers including Polyester (PET), Viscose/Rayon, Polypropylene (PP), and 100% bio-based Polylactide (PLA). Additionally, our high-performance technical workshops process inorganic and specialized fibers including high-modulus Aramid, Pre-oxygenated Polyacrylonitrile (PAN) filaments, Glass fiber, pure Basalt mineral fibers, and Polyimide (PI) for extreme flame retardant and hot-gas filtration applications.
Can functional attributes, colorimetry, pattern, and hand-feel stiffness be customized under one roof?
Yes. The decisive operational strength of YDL Nonwovens is full vertical integration. Rather than shipping base rolls to third-party converters, we handle base fabric hydroentanglement, continuous offline vat dyeing, sizing (stiffness adjustments), screen printing, and chemical functional finishing in-house. We can customize properties such as dynamic water repellency, multi-hazard flame retardancy, far-infrared emission, anti-mite resistance, thermochromic visual feedback, or custom aesthetic color matching to tight Pantone standards.
How does your factory ensure lot-to-lot consistency and ISO 9001 compliance for high-speed converters?
Our production workflow is governed by an audited ISO 9001 Quality Management System. Each master roll is continuously evaluated via automated in-line beta gauges for cross-web basis weight (GSM) consistency and high-speed optical vision systems that identify pinholes, slubs, or color deviations. Physical samples from every slit batch undergo lab testing for tensile elongation (MD/CD), hydrostatic head, liquid absorption capacity, and air permeability, with full Certificate of Analysis (CoA) documentation supplied per shipment.
Where is the primary factory located, and how does the logistics team handle international container shipments?
Our primary production complex is situated in Changshu, Jiangsu Province, China, giving us rapid intermodal access to the international ports of Shanghai and Ningbo. Since 2007, our export operations have serviced leading brands across North America, Europe, East Asia, and the Middle East. Rolls are wrapped in high-tensile waterproof packaging, mounted on heavy-duty cores, and container-loaded using specialized roll cradles to prevent ovalization and transit moisture absorption.
What is the standard procedure to request custom fabric prototyping, technical data sheets, or sample swatches?
Clients can initiate technical projects by communicating target specifications—including desired fiber composition, GSM target (typically 30 to 200+ gsm), web pattern (plain, mesh/apertured, embossed), tensile requirements, and functional chemical finishes—directly to our engineering team at [email protected]. We prepare sample swatches and complete technical data sheets (TDS) for converter qualification.
Functional & Specialized Range
Advanced Finishing & Functional Innovations
Review our specialized array of anti-mite, aromatic, pre-oxygenated, dyed, and responsive color-changing textiles.
China Fragrant Spunlace Nonwoven Fabric Products Manufacturers, Product
View Specifications
High-Quality Anti-mite Spunlace Nonwoven Fabric Product Factory, Factories
View Specifications
China Noctilucent Spunlace Nonwoven Fabric Products Companies, Product
View Specifications
China Pre-Oxygenated Filament Spunlace Nonwoven Fabrics Manufacturer, Suppliers
View Specifications
High-Quality Black Polyester Spunlace Nonwoven Fabric Products Factory, Products
View Specifications
High-Quality Off-line Dyed Spunlace Nonwoven Fabric Products Manufacturers, Factories
View Specifications
China Parallel Spunlace Nonwoven Fabrics Suppliers, Companies
View Specifications