Direct Converter Inventory · Tier-1 Substrates
High-Performance Engineered Appearance Substrates
Explore hydroentangled, laminated, and functionally finished rolls designed for medical draping, beauty masking, and high-tensile composite backing.
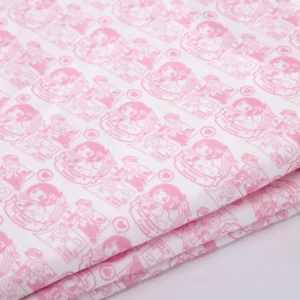
Precision Printing Spunlace Nonwoven Fabric
View Specification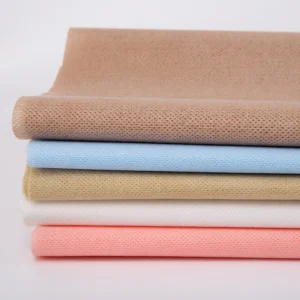
Engineered Mesh Spunlace Nonwoven Fabric
View Specification
Tactile Embossed Nonwoven Substrates
View Specification
Film-Laminated Spunlace Barrier Fabric
View Specification
Conductive Anti-Static Spunlace Solutions
View Specification
High-Tenacity Filament Spunbond Material
View Specification
Bi-Directional Spandex Elastic Spunlace
View Specification
Technical White Paper & Market Dynamics
The Evolution of Surface Morphology in Nonwoven Engineering
Modern industrial supply chains no longer view nonwovens as static roll goods. Surface appearance defines interfacial resin bonding, tactile consumer perception, and mechanical boundary dynamics.
2007
Specialized Production Established in Jiangsu
100%
In-House Carding, Dyeing, Sizing & Slitting
ISO 9001
Certified Closed-Loop Quality Control Standard
< 1.5%
Cross-Directional Tensile Variance Ratio
Interfacial Matrix Anchoring
In high-grade polyurethane (PU) and polyvinyl chloride (PVC) synthetic leathers, roll-to-roll surface morphology directly governs peeling resistance. In-house sizing controls chemical viscosity and mechanical anchoring, eliminating micro-delamination under extreme cyclical flex fatigue.
Micro-Fluidic & Capillary Kinetics
By engineering apertured meshes (from 16-mesh to 40-mesh configurations), spunlace structures dictate fluid intake velocity, liquid retention, and wiping friction coefficients. Optimal fiber entangling suppresses surface linting while accelerating liquid dispersion.
Smart Adaptive Surface Finishes
Transitioning beyond passive visual attributes, advanced functional finishing integrates thermo-responsive thermochromic microcapsules, UV-responsive phototropic dyes, and anti-static matrices directly into the web structure without degrading hand drape or fiber breathability.
Global Supply Resilience · Regulatory Frameworks
Regulatory Compliance & Localized Technical Support
Ensuring cross-border supply chain security through verifiable documentation, standardized chemistry, and localized compliance execution.
REACH, RoHS & OEKO-TEX Standard 100
All aqueous dyes, sizing binders, and anti-static chemicals meet rigorous EU and North American safety thresholds. Zero banned azo colorants, free formaldehyde, heavy metals, or hazardous alkylphenol ethoxylates (APEOs) enter the hydroentanglement lines.
ISO 9001 Batch Traceability
Every individual master roll and slit pack features full digital traceability back to incoming raw fiber lots (PET, Viscose, PP, PLA). Continuous optical inspection systems eliminate pinholes, oil specks, and slubs during high-speed hydroentanglement.
On-Site Converting Optimization
Our sales engineering specialists work alongside automotive tier-suppliers, medical converters, and filtration plants to calibrate tension profiles, slitting edge profiles, and adhesive curing cycles, ensuring seamless integration on your production machinery.
Field Deployment Case Architectures
Engineered Morphological Solutions Across Global Industries
Real-world integration of engineered appearance spunlace nonwovens across demanding consumer and industrial verticals.
Automotive Interior Synthetic Leather
Dyed and sized spunlace acts as the dimensional backer for automotive seating, dashboard wraps, and door card trims. Sizing prevents strike-through of liquid polyurethanes while retaining 4-way isotropic stretch under high-pressure thermoforming dies.
Cosmetic Face Masks & Skincare
Engineered apertured mesh structures paired with PLA and high-purity viscose provide skin-clinging drapery and serum reservoirs. Zero chemical binders eliminate facial irritation, providing ultra-clean, transparent wet layups.
High-Precision Cleanroom Wiping
Micro-embossed, ultrasonic-drilled nonwovens capture sub-micron particulates without surface marring in semiconductor and optical lens assembly. Continuous fiber entanglement prevents shedding under solvent exposure.
Forward Engineering Horizon
Material Science Roadmap: Next-Gen Functional Morphology
Our long-term R&D investments bridge polymer synthesis, computational water jet fluidics, and sustainable bio-based chemistries.
Phase 1: Present
Zero-Binder Monofilament Hydroentanglement
Standardizing cross-lapped carding lines with closed-loop water recirculation systems, achieving sub-1.2 MD/CD tensile ratios for isotropic strength across all converter lines.
Phase 2: 2025-2026
Circular Bio-Polymers & PLA Morphologies
Scaling biodegradable poly(lactic acid) and marine-degradable cellulosic matrices configured with ultrasonic apertures, replacing fossil synthetics in single-use beauty and hygiene markets.
Phase 3: 2026-2027
Stimuli-Responsive Nanocoatings
Developing ultra-thin functional polymer coatings that change opacity or color based on thermal thresholds and chemical saturation, creating visual indicator wipe substrates.
Phase 4: Future
Carbon-Neutral Performance Textiles
Closed-loop dyeing with recycled wastewater streams, low-energy drying cylinders, and post-consumer recycled PET (rPET) base materials verified under global recyling standards (GRS).
Functional & Specialized Morphologies
High-Tenacity & Smart Response Nonwovens
From thermochromic color shifts to flame-retardant pre-oxygenated fibers, our specialty product range meets critical technical specifications.
Powder-Dusted Spunlace Nonwoven Fabric
View Specification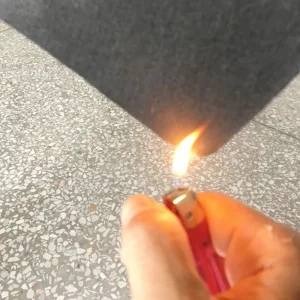
High-Temp Flame Retardant Spunlace
View Specification
Ultrasonic Drilling Patterned Nonwoven
View Specification
Photosensitive Color-Changing Spunlace
View Specification
Pre-Oxygenated Filament Thermal Barrier
View Specification
Standard Parallel Carded Spunlace Nonwoven
View Specification
Apertured Porous Mesh Spunlace Material
View Specification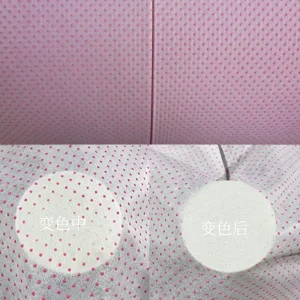
Dynamic Thermochromic Functional Spunlace
View Specification
Technical & Procurement FAQ
Frequently Asked Questions by Industrial Sourcing Teams
Direct technical answers regarding polymer configurations, minimum order parameters, quality assurances, and custom morphology finishing.
What parameters define "Appearance" in hydroentangled spunlace nonwovens?
In our manufacturing facility, appearance represents both macroscopic visual texture and microscopic fiber morphology. This encompasses aperture pattern geometries (such as plain, 22-mesh, 30-mesh, hexagonal, and pearl embossed patterns), chromatic finishes (pigment printing, vat dyeing, paste sizing), and micro-topographical uniformity. These factors determine air permeability, tensile modulus, liquid capture efficiency, and adhesion when used as synthetic leather backing cloth.
How does YDL Nonwovens control roll-to-roll color fastness and print resolution?
Because base web hydroentanglement, sizing, printing, and drying are fully integrated in our Changshu mill, our technical engineers regulate aqueous dye bath concentrations and curing oven temperatures on-line. Color fastness to dry and wet crocking complies with AATCC standards, preventing bleed or rub-off during converting, laminating, or secondary solvent exposure.
Can synthetic leather manufacturers customize stiffness and tensile elongation?
Yes. By formulating custom sizing resins (ranging from soft acrylics to stiff vinyl acetate copolymers) and adjusting web cross-lapping angles, we calibrate cross-directional (CD) and machine-directional (MD) elongation. This provides synthetic leather coaters with dimensional stability that resists curling or tearing under high line-tension PU/PVC knife coating.
What raw staple fibers can be processed for appearance and functional applications?
We process standard high-tenacity polyester (PET), semi-dull and bright viscose (rayon), polypropylene (PP), and biodegradable polylactide (PLA). For high-performance and thermal protective applications, we engineer specialized webs incorporating pre-oxidized polyacrylonitrile (PAN), alkali-free E-glass fibers, basalt filaments, and polyimide (PI) fibers.
What quality management and compliance standards govern your manufacturing?
Our complete manufacturing operation is certified under ISO 9001:2015. Raw fiber bales undergo optical purity screening, online camera detection identifies slubs and foreign matter during high-speed water entanglement, and all chemical sizing compounds comply fully with EU REACH and RoHS restrictions.
What are the lead times and sampling procedures for custom engineered rolls?
Standard master roll sample swatches and A4 technical prototype hand-sheets ship within 3 to 5 working days. Custom pilot trials (custom color matching, proprietary embossed mesh roll engraving, or specialized chemical treatments) generally complete within 2 to 3 weeks upon final technical sign-off.