Specified Nonwoven Grades Engineered for Australian Deployment
Engineered to deliver high cross-directional integrity, chemical inertness, and superior fluid absorption profiles for commercial converters across Sydney, Melbourne, Brisbane, and Perth.
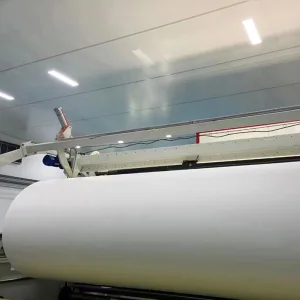
Australia Standard White Viscose Spunlace Nonwoven Fabric
View Specifications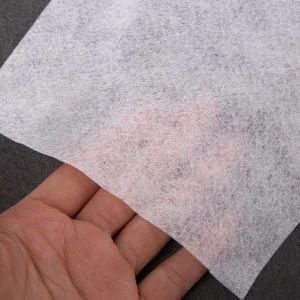
Australia Mining & Civil White Polyester Spunlace Nonwoven
View Specifications
Australia Eco-Pack Natural Bamboo Fiber Spunlace Nonwoven
View Specifications
Australia High-Efficiency PTFE Nonwoven Filtration Media
View SpecificationsAustralia & Global Material Supply Dynamics
Analyzing procurement vulnerabilities, structural cost pressures, and the operational realignments driving Sino-Australian B2B industrial collaborations.
Australian Domestic Realities
The Australian domestic market faces significant manufacturing bottlenecks characterized by high energy costs, expensive domestic haulage, and limited capacity in continuous upstream synthetic fiber production. Australian brand owners, medical converters, and mining infrastructure groups rely heavily on resilient offshore suppliers capable of meeting stringent AS/NZS compliance metrics without crippling cost premiums.
Global Capacity & Decarbonization
Globally, the technical nonwovens sector is executing a major transition toward circular economy polymers and low-VOC functional finishes. While European supply chains struggle with feedstock instability and North American production centers handle high domestic backlogs, China's advanced manufacturing hubs lead high-volume hydroentanglement output with embedded low-carbon supply pipelines.
Supply Chain Diversification
Australian corporate procurement mandates prioritize supply-chain continuity and reduced single-origin risk. Sourcing from large-scale, vertically integrated mills in Jiangsu, China offers an optimal combination: direct access to world-class petrochemical fiber streams, complete in-house customization, and immediate proximity to high-frequency marine shipping lanes directly servicing Botany, Melbourne, and Fremantle.
Engineering Advantages of Vertical Production in China
Eliminating subcontracting variance through synchronized base fabric formation, continuous dyeing, sizing, and multi-functional chemical treatments.
One-Roof Production Architecture
Operating a closed-loop ecosystem spanning fiber opening, precision cross-lapping, high-pressure hydroentanglement, continuous stenter drying, slitting, and inspection. By controlling web consolidation and finishing on a single production campus, our mills eliminate inter-subcontractor delays, material damage, and lot-to-lot inconsistencies.
ISO 9001 Process Discipline
Quality control begins at raw fiber intake—measuring denier, staple length, and moisture regain—and continues through online laser surface inspection systems that detect pinholes, slubs, and density variations. Every production master roll is tagged with full traceability data, ensuring compliance with Australian import auditing standards.
Advanced Chemical Functionalization
Beyond mechanical hydroentanglement, our facility incorporates in-line chemical pad-dry-cure finishing. We engineer hydro-phobic fluid barriers, durable flame retardancy, antistatic treatments, and specialized color formulations to exact engineering specs, cutting down lead times compared to typical third-party converting chains.
Material Engineering & Application Standards
Comprehensive technical metrics comparing substrate chemistries, basis weights, and target operational criteria for Australian industrial converters.
| Material / Chemistry | Available GSM | Tensile MD:CD Ratio | Core Performance Metric | Australian Application Focus |
|---|---|---|---|---|
| 100% Viscose / Rayon | 35 – 120 gsm | ~ 1.8:1 to 2.5:1 | Instant fluid absorbency, lint-free, pure cellulosic base | Medical drapes, healthcare wipes, clinical dressings |
| Polyester (PET) Spunlace | 40 – 250 gsm | ~ 1.5:1 to 2.2:1 | High mechanical strength, chemical resistance, thermo-stability | Civil geotextiles, industrial wipe rolls, automotive trim |
| PTFE Nonwoven Matrix | 100 – 450 gsm | Balanced Isotropic | Extreme temperature resistance (260°C), inert to acids/alkalis | Mining flue-gas filtration, smelter baghouses, chemical plants |
| Polyester / Bamboo Blends | 45 – 100 gsm | ~ 2.0:1 | Natural bacteriostatic profile, skin-neutral, eco-positioned | Commercial washroom systems, luxury hygiene converters |
| Flame-Retardant PET | 60 – 220 gsm | ~ 2.2:1 | Self-extinguishing (AS/NZS 1530 compliant), low smoke generation | Mine site accommodation interlinings, rail and aircraft upholstery |
| Aramid & Carbon Nonwovens | 80 – 350 gsm | Reinforced Multi-axial | Structural reinforcement, thermal barrier up to 400°C | Heavy resource sector protective equipment, composites, shields |
Targeted Applications Across Australian Industry
Meeting harsh environmental parameters, regulatory demands, and rigorous mechanical specifications throughout the Australian territory.
Pilbara & Hunter Valley Mining
Extreme thermal exposure, abrasive silica particulate, and aggressive process chemicals demand filtration media engineered to perform without degradation. Our high-denier PTFE, aramid, and basalt nonwoven filter fabrics deliver dependable dust-cake release and survive continuous thermal stress across mineral processing, smelting, and conveyor transfer points.
Hospitality & Clinical Healthcare
Meeting cleanroom expectations across Australian private hospital networks and primary clinics requires nonwoven substrates with near-zero lint generation, precise liquid dispersal, and biocompability. Our medical-grade viscose and polyester formulations integrate smoothly with local Australian roll-slitting, converting, and saturation packaging operations.
Infrastructure & Civil Engineering
Major transport, rail corridor, and water reservoir projects across Queensland, Victoria, and New South Wales require durable separation and filtration layers. Our engineered spunlace and synthetic technical membranes provide high puncture resistance, ultraviolet resistance, and controlled porosity to stabilize variable Australian subsoils.
Strategic Trends Shaping Enterprise Supply Agreements
Key risk management, sustainability, and logistics protocols modern procurement officers must evaluate when executing China-to-Australia material contracts.
Accelerated Lead-Time Pipelines
Managing Australian safety stocks requires minimal shipping variance. Leveraging direct deep-water container lanes out of Shanghai and Ningbo gives Australian procurement directors predictable 12 to 18-day port-to-port ocean transits, sharply reducing working capital tie-up compared to traditional trans-Pacific or trans-European freight routes.
Sustainable & Circular Mandates
Australian corporate sustainability guidelines and packaging packaging targets (APCO) drive demand for responsibly sourced raw materials. We supply full Chain of Custody (CoC) viscose, compostable PLA alternatives, and GRS-certified recycled polyester (rPET) fibers, supported by transparent lab verification records.
Tighter Technical Toll Manufacturing
Enterprise buyers are transitioning away from commodity catalog sourcing toward custom engineering. With our on-site laboratory testing, clients define fiber blends, moisture profiles, aperture patterns, and release characteristics that remain strictly consistent across multi-year delivery cycles.
Specialized & Functional Engineered Substrates
Engineered for high-stress filtration, fire-retardant barriers, precision dyeing, and heavy-duty composite applications across Australia.
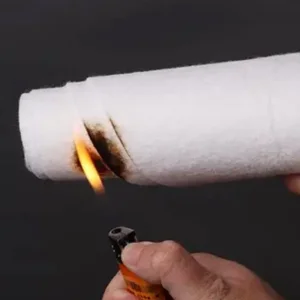
Australia Standard Fire-Resistant Polyester Nonwoven Fabric
View Specifications
Australia Circular Economy Recycled Polyester (rPET) Spunlace
View Specifications
Australia High-Spec Carbon Fiber Technical Nonwoven Fabric
View Specifications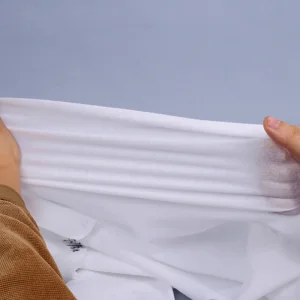
Australia Flex-Recovery Elastic Spunlace Nonwoven Fabric
View Specifications
Australia Pure Cotton Water-Stitch Hydroentangled Nonwoven
View Specifications
Australia Deep-Black Viscose Spunlace Nonwoven Fabric
View Specifications
Australia Heavy-Duty Black Polyester Spunlace Nonwoven
View Specifications
Australia Extreme High-Heat Aramid Nonwoven Barrier Fabric
View SpecificationsFrequently Asked Procurement Questions
Clear, direct responses to critical sourcing, compliance, logistics, and quality assurance questions for the Australian industrial market.
How do your nonwoven materials align with Australian import standards and technical certifications?
What typical shipping lead times can Australian buyers expect from your Jiangsu manufacturing center?
Can fiber blends and physical fabric attributes be tuned to custom downstream converting machines?
What Minimum Order Quantities (MOQs) and trial sample validation options are available?
How do you guarantee batch-to-batch color stability and tensile consistency across large recurring shipments?
Initiate Your Custom Material Sourcing Project
Connect with our senior nonwoven application engineers. Receive detailed technical datasheets, full compliance portfolios, and free pilot sample rolls tailored directly to your commercial specifications.