High-Performance Surface & Functional Spunlace Solutions
Explore custom-engineered roll goods processed with advanced carding, hydroentanglement, dusting, and multi-axis finishing lines.
The Paradigm Shift in Spunlace Engineering: Decarbonization & Functionalization
The global spunlace non-woven fabric ecosystem is experiencing unprecedented evolution driven by rigorous sustainability mandates, synthetic polymer substitution, and high-performance cross-lapping integration.
Circular Economy & Fossil-Free Matrixes
Global procurement directives (such as the EU Single-Use Plastics Directive) have catalyzed massive transition toward biodegradable alternatives. Our production matrix incorporates FSC-certified viscose, bamboo fiber, and 100% polylactic acid (PLA) alongside GRS-certified Recycled Polyester (rPET), closing the environmental lifecycle without compromising isotropic tensile integrity.
High-Density Hydroentanglement Hydraulics
Modern industrial converting demands exact fiber entanglement density. By employing multi-stage ultra-high pressure water needle heads operating at up to 250 Bar, mechanical bonding locks staple filaments with zero chemical binders. This yields unmatched low-linting characteristics, superior wet-expansion ratios, and skin-neutral dermatological safety profiles.
Functional Surface Impregnation
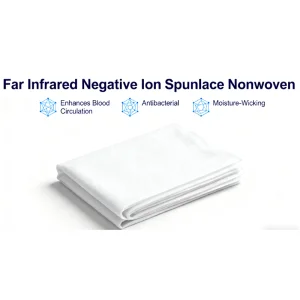
Moving beyond standard wipes substrates, high-value manufacturing incorporates smart finishes directly within the continuous hydro-process. From far-infrared negative ion doping, anti-mite encapsulation, to thermochromic pigments, technical nonwovens now act as responsive membranes for automotive interiors, medical isolation, and intelligent filtration.
Addressing Global Enterprise Sourcing Complexities
Enterprise procurement specialists in North America, Europe, and Asia-Pacific face rigorous challenges regarding web uniformity, tensile anisotropy, and supply continuity. Here is how our engineered solutions mitigate procurement risks.
| Procurement Challenge | Underlying Root Cause | YDL Nonwovens Engineering Solution | Measurable Quality Deliverable |
|---|---|---|---|
| MD/CD Tensile Disparity | Unbalanced parallel carding creates machine-direction bias and cross-direction web tear. | Full-cross lapping technology with calibrated draft-ratio control across five-cylinder carding engines. | MD:CD strength ratio optimized down to 1:1 to 1.3:1 for isotropic dimensional stability. |
| Binder Leaching & Chemical Linting | Residual PVA or acrylic adhesives degrade under chemical solvents or autoclaving. | 100% mechanical hydroentanglement using deionized, continuously filtered recirculated water jets. | Zero binder discharge; compatible with aggressive IPA, ethanol, and solvent matrices. |
| Substrate Delamination in Faux Leather | Poor resin saturation between web core and polyurethane (PU) skin layer. | Targeted sizing treatments and surface drop-plastic texturing with dialed pore distribution. | Peel strength increased by over 35% under ASTM D903 industrial standards. |
| Thermal Degradation in Filtration | Polyester and polypropylene fail under sustained flue gas temperatures above 150°C. | Processing of specialized polymers including Polyimide (PI), Basalt fibers, and Pre-Oxygenated PAN. | Continuous thermal stability up to 260°C with exceptional acid-alkali durability. |
Multi-Sector Turnkey Material Systems
Vertical manufacturing ensures full control over substrate thickness, fiber fineness (0.8D to 3.0D), embossing architecture, and customized post-treatments.
Medical Barrier & Surgical Assemblies
Engineered spunlace rolls featuring composite water-repellent (hydrophobic) and alcohol-repellent chemistries, meeting EN 13795 and AAMI Level 3/4 standards. Breathable yet impervious to fluid splashes, our medical-grade substrates offer ultra-low particulate shedding for clean surgical gowns, fenestrated drapes, and advanced wound dressing carriers.
Automotive & Synthetic Leather Substrates
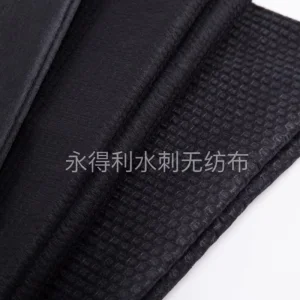
Doped-dyed black polyester and viscose matrices precision-sized to regulate resin absorption. Our drop-plastic and full-cross spunlace materials serve as high-strength backing fabrics for automotive seating, instrument panels, and luxury footwear, eliminating surface grain telegraphing while resisting micro-flex cracking.
Critical Cleanroom & Technical Filtration
From polyimide hot-gas dust extraction bags to semiconductor-grade lint-free dry wipes. Apertured mesh spunlace patterns maximize particulate holding volume without blinding air channels, providing consistent Darcy-law permeability and superior chemical inertness against harsh industrial effluents.
Localized Support & Global Compliance Framework
Ensuring frictionless supply chains and seamless regional compliance from our state-of-the-art Changshu production hub to worldwide shipping destinations.
Strict Quality Audits (ISO 9001:2015)
Every lot undergoes real-time optical web inspection for pinholes, basis weight variance (within ±2.5%), tensile modulus recording, and microbiological testing. Comprehensive Certificates of Analysis (CoA) accompany every container dispatch.
Global Environmental Compliance
Fully compliant with EU REACH Annex XVII, RoHS directives, OEKO-TEX Standard 100 Class I (safe for infant contact), and SVHC-free verification. Our functional chemical finishes are water-based, solvent-free, and heavy-metal-free.
Customized Converting & Logistics
Slitting from 50mm up to 3200mm roll widths with tailored core diameters (3-inch / 6-inch), heavy-gauge anti-static shrink wrapping, moisture-barrier palletizing, and multimodal container optimization serving global ports seamlessly.
Engineering the Future: Spunlace Roadmap 2026–2030
Continuous investment in next-generation web formation, nano-composite spinning, and closed-loop hydraulic recycling systems.
Phase 1: Sub-Denier Microfiber Entanglement
Developing 0.5–0.8 Denier sea-island split conjugated spinning spunlace. By splitting micro-filaments during high-pressure water impacts, web surface contact area multiplies threefold, creating ultra-luxurious suede-hand touch and high-filtration HEPA media.
Phase 2: Closed-Loop Zero-Discharge Water Systems
Upgrading multi-stage membrane bioreactors (MBR) and reverse-osmosis filtration across all high-pressure water jet manifolds. Target: 98.5% process water recycling rate with zero process effluent discharge by Q4 2026.
Phase 3: Smart Bioactive & Responsive Nonwovens
Commercializing integrated microencapsulated delivery systems for active skincare release, temperature-adaptive cooling webs, and inherent phosphorus-nitrogen flame-retardant staple webs that surpass standard UL94 V-0 flame spread criteria.
Custom Spunlace Engineering FAQ
Direct technical answers for converting plant managers, product designers, and global procurement teams.
What is the fundamental difference between parallel and cross-lapped spunlace?
Parallel-lapped spunlace aligns fibers predominantly in the machine direction (MD), providing high longitudinal pull strength and rapid production speeds, ideal for wet wipes. Cross-lapped spunlace folds carded webs diagonally, equalizing fiber direction to achieve near 1:1 MD:CD tensile balance, essential for medical gowns, technical coating substrates, and synthetic leather backing.
How does YDL achieve functional finishes without weakening hydroentangled webs?
Unlike thermal processes that degrade fiber molecular chains, YDL integrates specialized foulard impregnation, foam coating, and kiss-roll application stations directly in-line prior to drying. This ensures uniform chemical uptake (antistatic, flame retardant, repellent) without fracturing water-entangled mechanical interlocks.
Can you manufacture customized aperture meshes and embossed logos?
Yes. By utilizing custom patterned nickel sleeves and structured hydroentanglement drums, we manufacture standard mesh formats (10 to 40 mesh), pearl embossing, hexagonal patterns, and proprietary customer watermarks directly during hydraulic bonding.
What minimum order quantities (MOQ) and lead times apply for custom batches?
Standard white base fabric rolls carry an MOQ of 1,000 kg. Custom functional finishes, solution-dyed shades, or proprietary fiber blends (e.g., polyimide, basalt, pre-oxidized) typically require 2,000–3,000 kg. Standard trial sampling takes 3-7 business days, with volume orders dispatched in 15-20 days.
Advanced Structural & Specialty Fiber Spunlace Products
Engineered technical solutions including high-temperature polymers, full-cross alignments, dyed-in-mass substrates, and bioactive finishes.