2007+
Dedicated Spunlace Manufacturing Experience
ISO9001
Certified Stringent Quality Assurance Mill
100%
Vertical Integration (Fiber to Functional Finish)
50+
Global Export Markets & OEM/ODM Clients
Product Catalog I
High-Performance Functional & Technical Spunlace Grades
Explore our industrial-grade, thermal-responsive, and high-performance hydroentangled nonwoven roll goods tailored for global tier-one supply chains.
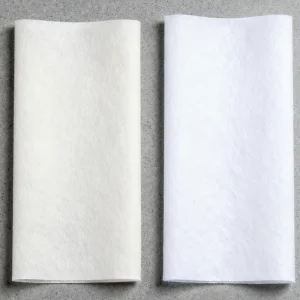
China Fluorescent Whitening Spunlace Nonwoven Fabric
View Details
China White Viscose Spunlace Nonwoven Fabric Products
View Details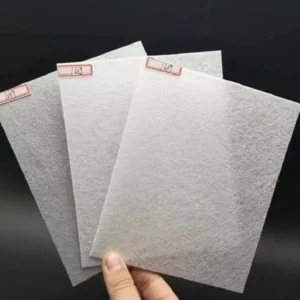
High-Quality Glass Fiber Nonwoven Fabric Solutions
View Details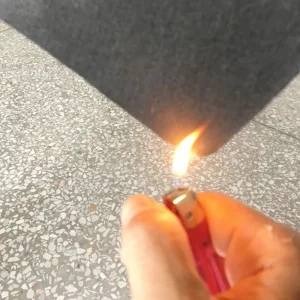
Flame Retardant Spunlace Nonwoven Fabrics
View Details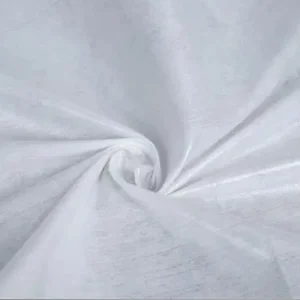
China Parallel Spunlace Nonwoven Fabrics
View Details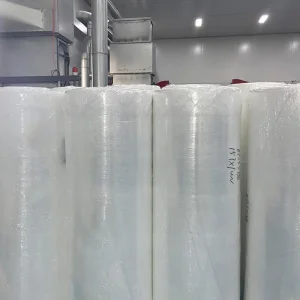
Semi-Cross Lapped Spunlace Nonwoven Substrates
View Details
High-Quality Film Laminated Spunlace Fabric
View Details
Executive Engineering Overview
Advanced Spunlace Hydroentanglement Principles & Metallurgy
Deciphering the thermodynamic, hydrodynamic, and mechanical advantages of high-pressure fluid entanglement across modern nonwoven industrial applications.
Hydrodynamic Entanglement
Spunlace technology relies on high-velocity micro-water needles (pressures exceeding 150 to 300 bar) directed through precision micro-perforated strip manifolds. These hydraulic jets pierce carded staple fiber webs, causing individual filaments to twist, coil, and frictionally interlock in a 3D isotropic matrix without chemical resins.
Zero-Binder Ecological Matrix
Unlike thermal bonding or chemical dip impregnation that introduce acrylic latexes, hydroentanglement produces an inherently pure fabric. The mechanical friction lock between fibers guarantees lint-free durability, clinical hypoallergenic safety, skin compatibility, and structural stability under extreme organic solvent wipe exposure.
Balanced MD:CD Tensile Dynamics
By modulating cross-lapping velocity, draft cylinder draw ratios, and jet impact angles, Yongdeli engineers achieve near 1:1 Machine Direction (MD) to Cross Direction (CD) tensile ratios. This eliminates web elongation deformation during synthetic leather polyurethaning, slitting, and converting operations.
Strategic Value Proposition
Why Tier-1 Global Procurement Selects China Spunlace Mills
Combining complete regional raw material availability with deep nonwoven clusters and vertically integrated secondary converting lines in Jiangsu Province.
Upstream Petrochemical & Bio-Fiber Hub
China's Yangtze River Delta hosts the world's dense cluster of virgin PET, modified hollow conjugate polyester, premium regenerated cellulose viscose, and high-purity PLA fibers. YDL benefits from instantaneous bale access, strict fiber tenacity selection, and insulated freight costs.
In-House Finishing Under Single Roof
Unlike standard trading operations or fragmented job-shops, Changshu Yongdeli Spunlaced Non-woven Fabric Co., Ltd. (YDL) runs base nonwoven lines, pad-dyeing ovens, aqueous sizing baths, rotary flexographic printing, and chemical bath treatments under unified ISO 9001 governance.
Comprehensive International Compliance
Every lot exported complies with rigorous international directives, including EU REACH SVHC restrictions, RoHS directives, OEKO-TEX Standard 100 toxicity thresholds, and cytotoxicity standards for medical grade drapes and wound contacts.
Production Excellence
End-to-End Production Process & Quality Engineering
A transparent breakdown of how raw staple fibers become world-class functional roll goods in our Changshu production facility.
Stage 01
Fiber Weighing & Opening
Bale management systems meter precise ratios of Viscose, PET, PP, or PLA. High-speed multi-stage spiked cylinder openers disentangle fibers into cloud-like consistency.
Stage 02
Double Doffer Carding & Lapping
Fine-wire carding teeth comb fibers into micro-thin parallel layers. Computer-regulated semi-cross or cross-lappers fold layers to set exact basis weight (GSM) and isotropic strength.
Stage 03
Multi-Stage High-Pressure Hydroentanglement
Successive low-to-high pressure de-aeration and jet manifolds inject ultra-pure filtered water, locking the web into plain, pearl-weave, or mesh/apertured designs.
Stage 04
Through-Air Drying & Heat Setting
Negative-pressure perforated drum driers remove moisture uniformly without crushing web loft, preserving softness, tensile resilience, and exact volumetric caliper.
Stage 05
Continuous Dyeing, Printing & Chemical Finishing
In-line foulard padding rolls introduce flame retardants, hydro-repellent fluorochemicals, antistatic additives, thermal dyes, or continuous gravure pattern prints.
Stage 06
Laser Inspection, Slitting & Clean Packing
Automated visual optical surface defect detectors scan 100% of the web for foreign particles, slubs, or holes before precision pneumatic razor slitting and moisture-barrier vacuum packaging.
Macro Sector Solutions
Engineering Specifications for Key Industrial Sectors
Cross-referencing technical polymer selections with real-world converting, regulatory, and mechanical demands.
| Target Sector | Material Composition | Basis Weight (GSM) | Functional Enabler | Primary Regulatory Focus |
|---|---|---|---|---|
| Medical & Healthcare | Viscose / PET Blend or 100% PP | 35 – 80 g/m² | Low-linting, fluid repellent, alcohol barrier | ISO 10993 Cytotoxicity, EN 13795 |
| Cosmetics & Facial Care | 100% Bamboo / Viscose / PLA | 30 – 65 g/m² | High liquid retention, skin-drape conformability | OEKO-TEX Class 1, EU Cosmetics Reg |
| Automotive Synthetic Leather | Microfiber PET / PA Blends | 60 – 220 g/m² | Tensile elasticity, heat-curing dimensional stability | VDA 270 Odor, FMVSS 302 Flammability |
| High-Temp Industrial Filtration | Polyimide (PI), Basalt, Glass Fiber | 100 – 450 g/m² | Continuous thermal barrier (up to 260°C+), acid proof | ISO 16890, EN 779 Air Standards |
| Household & Heavy Degreasing | Cellulose Pulp / Polypropylene | 45 – 110 g/m² | High oil-absorption ratio, tear-resistant aperture | BfR XXXVI Food Contact Compliant |
Market Foresight & R&D
Next-Generation Spunlace Technology Trends
Examining circular economy mandates, plastic-free wipes legislation, and technical industrialization.
EU Single-Use Plastics (SUP) Pivot
Global regulations are rapidly banning or taxing synthetic wipe substrates. YDL leads the transition by developing 100% biodegradable, home-compostable hydroentangled roll goods leveraging virgin lyocell, wood pulp blends, and certified polylactic acid (PLA) polymers that disperse seamlessly without microplastic residue.
Smart Responsive & Thermochromic Textiles
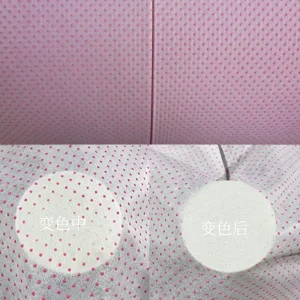
By compounding specialized micro-encapsulated thermochromic pigments and far-infrared emitters into functional binders, nonwovens can shift visual appearance upon thermal thresholds or stimulate blood circulation in therapeutic orthopedic wrap applications.
Advanced Water Recycling Closed-Loops
Modern hydroentanglement demands massive volumetric water flow. Yongdeli operates an industrial membrane bioreactor (MBR) and sand bed multi-cyclone water filtration system that recycles over 95% of process effluent, reducing freshwater consumption and lowering the carbon footprint per metric ton.
Procurement Directives
Procurement Strategy: RFQ Blueprint for Enterprise Buyers
Essential engineering parameters procurement directors must audit prior to placing high-volume container orders.
GSM & Dimensional Tolerances
Define acceptable basis weight variance (+/- 3% standard), roll slit width tolerance (+/- 1mm), maximum roll outer diameter (OD), core inner diameter (typically 76mm heavy-wall cardboard), and minimum continuous roll lengths without splice breaks.
Mechanical Tensile & Elongation
Specify minimum dry/wet breaking force (N/5cm) in both Machine Direction and Cross Direction. For automated web converters, CD elongation percentage at peak break is essential to prevent bottleneck jams during high-speed folding.
Chemical Extraction & Surface Energy
For wipes and medical drapes, verify total non-volatile residue (NVR), dynamic absorbency rate (seconds), water/oil holding capacity (%), and ensure surface tension matches target wetting solutions or polyurethane top-coatings.
Factory Engineering FAQ
Frequently Asked Technical & Sourcing Questions
Direct technical responses addressing common procurement, manufacturing, and logistical inquiries.
What is the core structural difference between parallel-laid and cross-lapped spunlace nonwovens?
Parallel-laid spunlace directs fibers predominantly in the machine direction, providing high MD tensile strength but significantly lower CD strength, optimal for basic wiping where longitudinal pull is dominant. Cross-lapped hydroentangled webs fold carded layers crisscross prior to jet entangling, ensuring an isotropic ratio approaching 1:1. This isotropic distribution prevents necking under tension, essential for medical gowns, technical filtration, and synthetic leather backing.
How does YDL maintain strict lot-to-lot color fastness and physical stiffness across large orders?
Because our pad-dyeing, sizing, and curing ovens are integrated directly into our Changshu manufacturing complex, our technical team monitors continuous spectrophotometer delta-E (dE < 0.8) color boundaries in real time. Sizing polymer baths undergo automated viscosity and temperature regulation to maintain uniform pick-up weight, avoiding shade drift or stiffness deviations across 40-foot HQ container batches.
Can you engineer functional spunlace with flame retardancy without degrading the soft drape?
Yes. We apply halogen-free organophosphorus or specialized water-based flame retardant formulations during the secondary foulard padding cycle, calibrated precisely to achieve vertical flame resistance (such as UL94 V-0 or NFPA 701) while retaining fiber flexibility. Our precise through-air tensionless curing process sets the chemistry without baking or stiffening individual staple filaments.
What specialty high-performance fibers can be spunlace-hydroentangled at your facility?
Beyond commodity polyesters and viscose, our carding and high-pressure jet manifolds are adapted to process specialized industrial filaments: glass fibers for structural insulation, basalt mineral fibers for extreme thermal and acoustic barriers, high-performance polyimide (PI) fibers for hot-gas filtration, and pre-oxidized polyacrylonitrile (PANOF) yarns for industrial arc flash or aerospace fire stops.
What is the standard production lead time and minimum order quantity (MOQ) for custom formulations?
Standard white base fabric specifications typically have an MOQ of 1,000 kg per trial run, while specialty functional treatments, pad-dyed custom Pantone matches, or custom-pattern printing runs start at 2,000 to 3,000 kg depending on target basis weight. Typical manufacturing lead time from raw fiber intake to containerized port delivery via Shanghai is 15 to 25 business days.
Product Catalog II
Advanced Specialty & Industrial Spunlace Nonwovens
Explore our advanced structural, decorative, composite, and high-tenacity hydroentangled fabrics engineered for extreme environments.
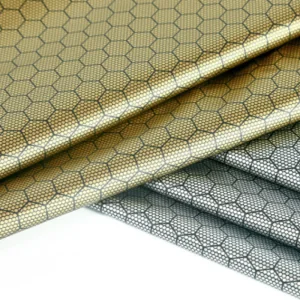
Gold & Silver Stamped Spunlace Fabric
View Details
Pure White Polyester (PET) Spunlace Nonwoven
View Details
Apertured Mesh Spunlace Nonwoven Fabric
View Details
High-Quality PTFE Nonwoven Technical Media
View Details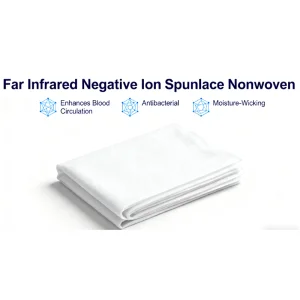
Far-Infrared Negative Ion Nonwoven Fabric
View Details
High-Tenacity Carbon Fiber Nonwoven Web
View Details
High-Quality Filament Spunbond Substrates
View Details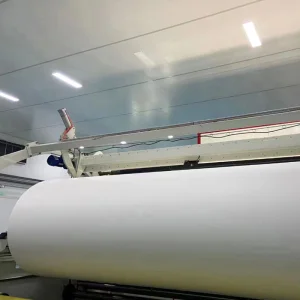
Microencapsulated Fragrant Spunlace Fabric
View Details
Direct Factory Sourcing
Accelerate Your Spunlace Engineering Pipeline
Connect directly with the YDL Nonwovens technical engineering team in Jiangsu, China. Request full technical data sheets (TDS), safety certifications, and customized trial sample swatches for your specific converting line.