High-Performance Technical Nonwoven Portfolio
Explore our specialized hydroentangled fabrics manufactured under ISO 9001 quality systems, featuring customized fiber blending, functional coatings, and precise physical performance profiles.
The Spunlace Nonwoven Manufacturing Process: Technical Metallurgy & Fluid Dynamics
A rigorous industrial perspective on how raw polymers and staple fibers are converted into high-tensile hydroentangled matrices through mechanical carding and high-pressure micro-fluidics.
Bale Opening & Weighing
Multi-component staple fibers (Viscose, PET, PP, PLA, and technical microfibers) undergo gravimetric dosing and ultra-fine mechanical opening. Automated multi-bale plucking ensures a homogenous blend with coefficient of variation (CV%) strictly kept below 1.2% across large batches.
High-Speed Carding & Lapping
Fibers travel through double-cylinder carding machines with worker-stripper rollers to parallelize individual filaments. Servo-controlled cross-lappers lay web layers at calibrated cross angles, fundamentally structuring the cross-directional (CD) to machine-directional (MD) tensile ratio.
Hydroentanglement
Micro-orifice strip injectors generate high-velocity laminar water needles ranging from 30 bar to 250+ bar. As water penetrates the unbonded web against micro-perforated or patterned drums, kinetic energy curls and interlocks fibers mechanically without chemical resins or thermal melting.
Vacuum Dewatering & Drying
High-efficiency slot vacuum boxes extract up to 75% of residual water before the fabric enters multi-cylinder through-air drying chambers. Controlled convective airflow preserves web loftiness, soft hand feel, and uniform density while preventing fiber collapse or surface glazing.
Functional Finishing & Dyeing
Inline or offline padding units apply target surface chemistries: hydrophobic/oleophobic fluorocarbon finishes, durable flame retardants (FR), quaternary ammonium antimicrobial agents, magnetic functional coatings, or thermochromic pigment dispersions matched to customer Pantone specs.
Automated Vision Inspection
Continuous line-scan cameras detect defects, dark specks, unbonded yarn fragments, and pinholes down to 0.1mm. High-speed center-surface winders slit master rolls to bespoke converter widths (100mm to 3200mm) with precision tension feedback controls.
Polymer Engineering & Fiber Performance Parameters
Quantitative benchmark of staple fiber formulations utilized across our Changshu manufacturing complex, showing physical properties and compliance benchmarks.
| Fiber Polymer Composition | Typical GSM Range | Tensile Strength (MD/CD N/5cm) | Fluid Absorption Capacity | Key Performance Attribute | Standard Certifications |
|---|---|---|---|---|---|
| Viscose / Polyester (70/30 or 50/50) | 35 - 120 g/m² | MD: 120-280 / CD: 95-210 | 850% - 1050% by weight | Ultra-soft hand feel, high liquid retention, lint-free | OEKO-TEX 100 REACH |
| 100% Polypropylene (PP) Microfiber | 30 - 80 g/m² | MD: 140-310 / CD: 110-240 | Oleophilic / Hydrophobic | Exceptional acid/alkali resistance, zero lint emission | FDA 21 CFR RoHS |
| Polylactic Acid (PLA) Corn Fiber | 40 - 90 g/m² | MD: 110-220 / CD: 85-170 | 650% - 800% by weight | 100% Industrially Compostable, mild skin-pH compatible | EN 13432 ASTM D6400 |
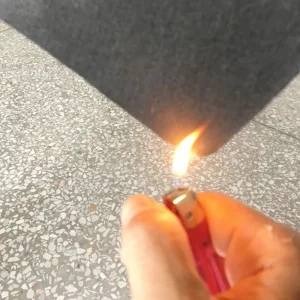
| Pre-Oxygenated PAN Fiber (PANOF) | 80 - 260 g/m² | MD: 240-480 / CD: 190-380 | Hydrophobic Barrier | LOI ≥ 45%, does not melt or drip under direct 800°C flame | UL94 V-0 FAR 25.853 |
| Continuous Filament Carbon / Basalt | 100 - 350 g/m² | MD: 550-980 / CD: 420-760 | Inert chemical substrate | Continuous thermal stability up to 650°C, EMI attenuation | ISO 14001 ISO 9001 |
China Supply Chain Advantages & Western Compliance Assurance
Combining the cost efficiencies of the Jiangsu textile industrial belt with strict global regulatory frameworks for zero-friction importing.
Direct Feedstock Proximity
Situated in Changshu within China's premier petrochemical and viscose synthesis cluster, raw staple polymers are sourced within a 60-mile radius. This eliminates upstream domestic transit volatility, reduces raw material holding costs, and guarantees uninterrupted production schedules even during seasonal raw-material peaks.
Full Vertical Integration
Unlike regional contract converters who outsource post-processing, our facility houses carding, hydroentanglement, continuous dying, high-speed rotary printing, calendering, and chemical functional dipping under one single roof. Eliminating subcontractor hand-offs yields total lot-to-lot traceability and decreases production cycle lead times by up to 40%.
Global Certification Guardrails
Every commercial roll is engineered to clear stringent EU REACH SVHC limits, US FDA 21 CFR (indirect food and medical grade contact), and OEKO-TEX Standard 100 Annex 6 Class I (safe for prolonged baby skin contact). Factory operations maintain formal audits under ISO 9001:2015 and ISO 14001 environmental frameworks.
End-Market Specific Spunlace Formulations
Custom hydroentangled nonwoven substrates optimized for high-speed downstream converting machines.
Medical & Surgical Devices
Non-linting, biocompatible substrates for surgical drape fenestrations, gowns, wound dressings, and blood-absorbent pads. Compatible with Gamma, EtO, and Steam autoclaving.
Cosmetics & Sheet Masks
Cupro, Lyocell, and 100% Viscose webs engineered with exceptional tensile wet strength, invisible transparency when saturated with serum, and minimal dripping.
Automotive PU/PVC Substrates
Specially sized and dyed backing fabrics designed for micro-porous polyurethane synthetic leather coating in car seat upholstery, door panels, and instrument wraps.
Thermal & High-Voltage Barriers
Carbon fiber, Basalt, and pre-oxidized polyacrylonitrile (PAN) spunlace fabrics providing non-conductive electrical insulation and flame-retardant thermal barriers in EV batteries.
Emerging Trends Reshaping the Global Spunlace Sector
Strategic technological pivots driving capital investments across our research laboratories and production lines.
Circular Economy & Plastic-Free Directives
In direct response to the EU Single-Use Plastics Directive (SUPD), our engineers have scaled 100% certified plastic-free, water-dispersible formulations using FSC-certified wood pulp blended with refined Lyocell. These disperse within municipal sewer systems under turbulent hydraulic action while maintaining complete wet tensile reliability during consumer wiping tasks.
AI-Assisted Closed-Loop Hydroentanglement
Water-jet injection pressure profiles are now automatically modulated via inline machine learning algorithms. By sensing real-time web thickness, fiber orientation variability, and water reflectance, the system dynamically adjusts pump frequency to reduce factory power consumption by 18% while keeping basis weight uniformity within a tight ±1.0 g/m² tolerance.
Active Surface Functionalization
Beyond traditional mechanical bonding, we are commercializing nanoscale coatings: microencapsulated fragrance release fabrics, phase-change materials (PCM) for cooling medical gowns, and cationic surface treatments for color-catcher laundry sheets capable of electrostatically trapping fugitive anionic dye molecules during high-temperature wash cycles.
Functional Finishing & Advanced Filament Nonwovens
Explore specialized industrial, flame-retardant, anti-static, and carbon-reinforced nonwoven fabrics manufactured to strict buyer specifications.
Frequently Asked Technical & Sourcing Questions
Direct answers from our senior materials engineering and international logistics divisions.
What is the fundamental engineering difference between spunlace and spunbond nonwovens?
Spunbond utilizes continuous filament extrusion where thermoplastic polymers (PP, PET) are melted, attenuated into filaments, laid randomly, and thermally bonded using heated calendar rolls. Spunlace (hydroentangled) processes staple, cut fibers (such as Viscose, Rayon, Cotton, PLA, or technical filaments) that are mechanically carded into a web and bonded via ultra-high-pressure micro-water jets. Spunlace yields superior drape, zero chemical residue, skin-soft hand feel, high liquid absorption, and cloth-like tactile qualities compared to the rigid, plastic-like texture of spunbond.
How does your factory control the MD:CD tensile strength ratio?
Standard parallel carding produces webs oriented primarily along the Machine Direction (MD), often exhibiting extreme tensile disparities up to 4:1 or 5:1 relative to the Cross Direction (CD). We utilize computer-synchronized cross-lapping machinery combined with variable-speed draft units and multidirectional hydraulic injection manifolds. This balances fiber orientation to engineer nearly isotropic ratios (MD:CD as low as 1.1:1 to 1.3:1), which is crucial for synthetic leather backings and high-speed rotary converting lines.
Can you manufacture custom surface aperture patterns and embossings?
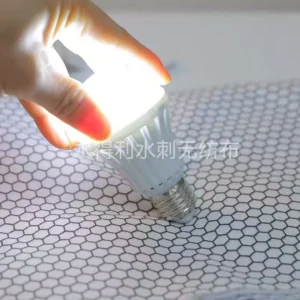
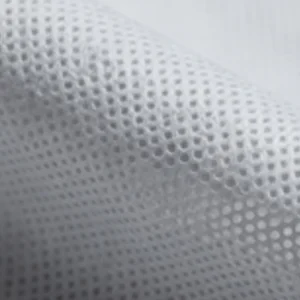
Yes. Our hydroentanglement lines support interchangeable patterning cylinders and nickel mesh sleeves. We regularly produce plain flat webs, 22-mesh/28-mesh apertured perforations (honeycomb, diamond, round hole), pearl weaves, EF jacquard textures, wave patterns, and branded custom watermark logos embedded directly into the fiber matrix during water-jet entanglement without compromising tensile integrity.
What documentation and compliance do you supply for European and North American customs clearance?
Every commercial container shipment is supported by complete traceability documentation: Full Certificate of Analysis (COA) specifying verified GSM, tensile, and moisture parameters; formal SDS sheets; EU REACH SVHC non-presence declarations; OEKO-TEX Standard 100 Annex 6 compliance proofs; and Bill of Lading accompanied by customs-validated Certificate of Origin (Form A, RCEP, or standard C/O) to optimize regional import tariff classifications.
What is your minimum order quantity (MOQ) and sample lead time?
For standard white conventional Viscose/Polyester blends, our commercial trial MOQ starts at 1,000 kg per specification, with full-scale production runs optimized at 3,000 kg (equivalent to one standard 20GP shipping container). For custom functional formulations (custom dyeing, flame-retardant dipping, or specialized fibers like pre-ox PAN or carbon fiber), MOQs range from 2,000 kg to 5,000 kg. Hand-sheet or roll samples from our automated pilot line can be dispatched within 5 to 7 business days.
How does your facility address water conservation and environmental wastewater treatment?
Hydroentanglement requires substantial water circulation. Our mill operates a closed-loop multi-stage water reclamation system featuring high-rate sand filtration, diatomaceous earth purification, and ultrafiltration (UF) reverse osmosis membranes. Over 96% of industrial process water is continually recycled back to the high-pressure water pumps, drastically reducing freshwater intake and ensuring zero non-compliant effluent discharges.
Accelerate Your Nonwoven Product Development Cycle
Consult with our materials science engineers to customize basis weight, fiber blending ratios, aperture patterns, and functional finishes tailored to your exact industrial requirements.