Primary Conversion Platforms
Engineered Baseline Processes for Victoria's Industrial Converters
Deploying hydroentanglement, chemical saturation, and thermal bonding processes calibrated for low-linting medical and durable manufacturing applications.
Filament Spunbond Nonwoven Fabric for Melbourne Infrastructure
Technical Details
Melbourne Semi-Cross Lapped Precision Spunlace Nonwovens
Technical Details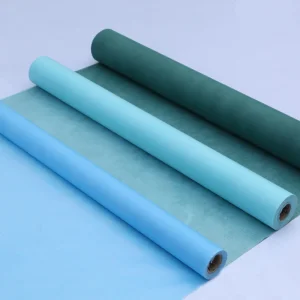
Chemical Bond Nonwoven Substrates for Melbourne Fabricators
Technical Details
Melbourne Industrial Ecosystem
Victoria's Transition: High-Value Advanced Manufacturing & Procurement Demands
Strategic analysis of cross-border manufacturing integration supporting Greater Melbourne's medical packaging, civil infrastructure, and advanced composite sectors.
100%
Binder-Free Options
±2.5%
GSM Uniformity Control
1:1
MD/CD Ratio Customization
ISO 9001
Verified Process Governance
Supply Chain Resilience
Local Victoria convertors in Dandenong, Campbellfield, and Altona face high operational cost structures. By delivering master rolls with certified structural consistency, we decouple local converting lines from supply bottlenecks, reducing waste downstream.
Therapeutic & Cleanroom Needs
Melbourne’s world-class biomedical precinct in Parkville demands medical-grade nonwovens adhering strictly to bioburden thresholds, particle shed prevention, and high fluid barrier standards (AS 4187 & EN 13795 compliance frameworks).
Civil Infrastructure Infill
Victoria's Big Build transport infrastructure projects mandate heavy-duty geotextile sub-bases with long-term mechanical puncture resistance, consistent elongation under dynamic load, and soil-pore filtration stability.
Technical Architecture
Process Control Standards & Mechanical Performance Matrix
A comparative overview of our continuous hydroentanglement and chemical formulation stages calibrated for Tier-1 supply chains.
| Process Route | Fiber Matrix Capability | Tensile Profiles (MD/CD) | Core Industrial Application (Melbourne) |
|---|---|---|---|
| Parallel Hydroentanglement | Viscose / Polyester, Bamboo, Pure Cotton | Oriented (MD > CD, ratio ~ 3:1) | Dry/Wet wipes, disposable medical packs, consumer facial pads |
| Full-Cross Spunlace Bonding | PET, Viscose, Microfiber, PLA blends | Isotropic Balance (MD:CD ~ 1:1 to 1.2:1) | Synthetic leather basecloth, acoustic wall interlinings, automotive |
| Continuous Filament Spunbond | 100% Virgin Polypropylene (PP), PET | High Elongation, Superior Tear Resist | Geotextiles, agricultural cover, structural mattress backing |
| Specialty Pre-Oxidized / Carbonized | PAN-based precursor, Basalt, Carbon filament | Zero Melting Point, High Thermal Index | Aviation fire barriers, battery separator mats, furnace insulation |
Future-Proofed Production
Biopolymer Evolution & Circular Economy Adaptation
Global environmental directives increasingly place nonwoven polymer substrates under strict scrutiny. For our Australian partners, the focus is squarely on transitioning away from fossil-based single-use plastics to certified compostable polymers.
Our production facilities have completed multi-phase engineering adjustments to process pure Polylactic Acid (PLA), certified Lyocell, and unbleached organic cotton fibers using closed-loop, ultra-filtered hydroentanglement water recycling systems that lower carbon intensity per metric ton by up to 28%.
Port of Melbourne Freight & Logistics Framework
- FCL / LCL Direct Despatch: Seamless container routes direct to DP World & Patrick Terminals at the Port of Melbourne.
- Export Moisture Control: Double-vacuum wrapped packaging with desiccants to survive ocean crossing moisture variations.
- Custom Core Diameters: 3-inch (76mm) and 6-inch (152mm) core adaptations to interface cleanly with standard Australian converting unwinds.
Full Process Capabilities
Specialty, Cross-Lapped, and Functional Nonwovens for Melbourne
Explore our deep process catalog spanning electrostatic absorption, flame barrier filaments, carbon fiber webs, and custom mesh aperturing.
Melbourne Full-Cross Spunlace Nonwoven Fabric Lines
Technical Details
Polypropylene Spunlace Solutions for Melbourne Manufacturing
Technical Details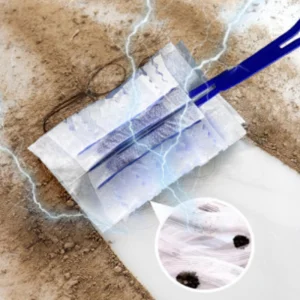
Melbourne Electrostatic Adsorption Spunlace Filtration Media
Technical Details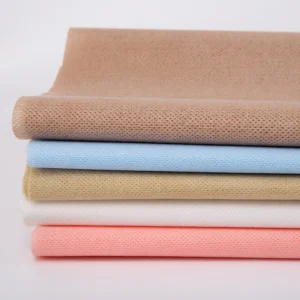
Engineered Mesh Apertured Spunlace for Melbourne Converters
Technical Details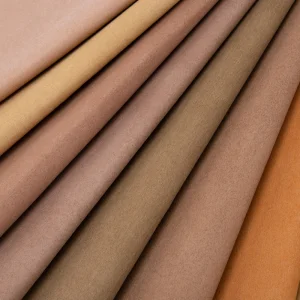
Melbourne Off-line Dyed Spunlace Industrial Fabrics
Technical Details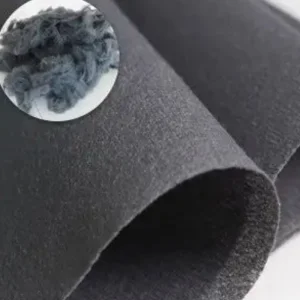
Carbon Fiber Nonwoven Web for Melbourne Advanced Composites
Technical Details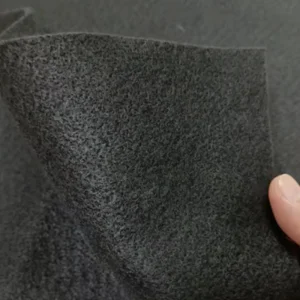
Melbourne Pre-Oxygenated Flame Barrier Spunlace Materials
Technical Details
Engineered Colored Fiber Nonwovens for Melbourne Designers
Technical Details
Procurement & Engineering FAQ
Addressing Sourcing Questions for Victorian & Global Buyers
Specific insights on cross-lapping mechanics, minimum roll orders, lead times, and regulatory compliance.
What are the key technical distinctions between parallel and cross-lapped spunlace nonwovens for Melbourne converters?
Parallel spunlace carding directs fibers in the machine direction (MD), leading to a high MD/CD tensile ratio (typically 3:1 to 4:1) with significant cross-directional elongation. This makes it ideal for cost-efficient consumer wipes where uniform CD tension is not critical. Conversely, cross-lapped spunlace folds carded webs diagonally, resulting in balanced MD:CD ratios (near 1:1 or 1.2:1). This provides multi-directional dimensional stability vital for synthetic leather substrates, automotive trim, and demanding medical barrier applications across Melbourne plants.
How do your production facilities manage lot-to-lot consistency and weight tolerance across large roll runs?
Our lines utilize real-time online beta-gauge radiometric scanning systems to continually map GSM distribution across the entire web width. Hydroentanglement water injection pressures are automatically regulated by closed-loop PLCs to compensate for localized bulk density fluctuations, maintaining weight variation within a strict ±2.5% tolerance window.
What documentation is provided to satisfy Australian customs and biosecurity regulations?
Every export shipment targeting Melbourne includes comprehensive Certificates of Analysis (COA), formal Mill Test Certificates validating tensile, GSM, and bioburden levels, fumigation/biosecurity declarations (where applicable for wooden pallet transit conforming to ISPM 15), and fully traceable batch documentation aligning with ISO 9001 governance.
What are your typical production lead times and Minimum Order Quantities (MOQ) for custom slit widths?
Standard baseline specifications carry an MOQ of 1 metric ton per custom formulation, while customized dyed, functional finished (FR, hydrophobic), or complex fiber blends typically require 3 to 5 tons. Factory processing time spans 15 to 20 days post-specification approval, followed by roughly 14 to 18 days maritime transit to the Port of Melbourne.
Can functional finishes (flame retardancy, anti-microbial, anti-static) withstand standard downstream converting?
Yes. Our functional chemistries are integrated via integrated pad-dry-cure and foulard systems rather than superficial spray treatments. This ensures durable chemical bonding throughout the porous 3D fiber network, preserving flame resistance (complying with standard AS/NZS flammability tests) and hydrophobic properties even after slitting, perforation, and downstream laminating processes.