Hydroentanglement Engineering Excellence Since 2007
High-Quality Spunlace Nonwoven Fabrics Manufacturer & Industrial Solutions
Precision-engineered, hydroentangled nonwoven substrates utilizing virgin, recycled, and technical fibers. Vertically unified from fiber carding to functional surface chemistry for global OEMs, medical convertors, and automotive tier-1 providers.
Primary Substrates & Functional Composites
Precision Catalog: Commercial Engineering Grades
Verified hydroentangled substrates designed for high-stress manufacturing lines, performance medical barriers, and technical synthetic laminates.
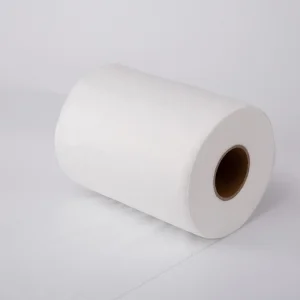
rPET Recycled Polyester Spunlace Nonwoven
Product Specifications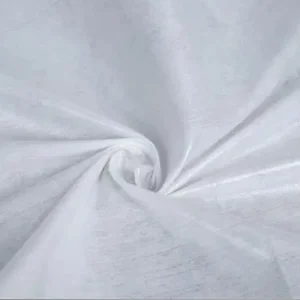
Parallel-Lapped High-Tensile Spunlace Web
Product Specifications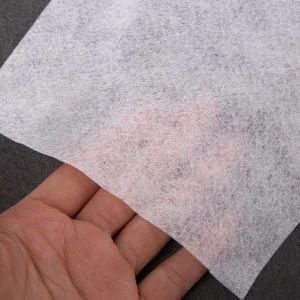
Optical White Virgin Polyester (PET) Substrate
Product Specifications
Rigid Chemical Bond Structural Nonwovens
Product Specifications
Dope-Dyed Colored Fiber Spunlace Matrix
Product Specifications
Semi-Cross Lapped Isotropic Spunlace Nonwoven
Product Specifications
Conductive Silver-Coated Shielding Nonwoven
Product Specifications
Technical White Paper
Hydroentanglement Mechanics & Physical Kinetics
A comprehensive examination of high-pressure fluid dynamics in binder-free web entanglement, MD/CD ratios, and micro-structural fiber interlocking.
Hydraulic Jet Kinetics
Hydroentanglement utilizes micro-water needles propelled at pressures between 40 and 200 bar through laser-drilled injector strips. As high-velocity fluid columns traverse the fibrous batt, momentum is transferred to individual staple fibers. The sudden deflection and rebounding of water off structural conveyor belts creates three-dimensional microscopic vortices, physically braiding fiber ends without thermal melting or chemical binder resins.
Isotropic Tensile Vectoring
Through advanced cross-lapping and semi-cross-lapping profiling, carded webs overcome traditional machine-direction (MD) bias. Standard parallel webs yield MD:CD tensile ratios of 4:1, which can compromise convertor slitting speeds. By precisely controlling the cross-lapper drafting carriage velocity relative to needle-punch delivery, our isotropic grades achieve balanced 1.2:1 MD:CD ratios, eliminating neck-in deformation in multi-layer lamination.
Delamination & Capillary Yield
Eliminating chemical binders creates high internal surface area and natural interstitial voids. The resulting open capillary structure delivers liquid retention factors up to 900% dry weight without structural matrix collapse. This chemical-free consolidation preserves natural staple softness, ensures skin biocompatibility, and provides the necessary fiber integrity for post-process surface functionalization.
Global Industry Solutions
Localized Applications & Strategic Performance Tiers
Engineered hydroentangled materials tailored to strict international regulatory frameworks and specialized converting demands.
Medical & Surgical Convertors
Engineered for surgical drapes, medical gauze, laparotomy sponges, and wound care backings. Substrates maintain strict bio-compatibility, near-zero lint generation (Helmke Drum testing compliant), and consistent hydrostatic head performance. Compatible with ethylene oxide (EtO), gamma irradiation, and steam autoclave sterilization cycles without polymer degradation.
PU/PVC Synthetic Leather Substrates
Specialized dyed and sized spunlace bases engineered for automotive interior trim, luxury footwear, and high-abrasion upholstery. Sizing finishes stabilize the fiber web against chemical swelling and high-temperature polyurethane coagulation troughs, delivering peel strengths exceeding 35N/3cm while eliminating the orange-peel surface defect common in low-tier base fabrics.
Advanced Filtration & Thermal Barriers
Manufactured using technical high-performance polymers including pre-oxidized polyacrylonitrile (PAN), meta-aramid, polyimide (PI), and basalt fibers. Engineered for hot gas filtration in waste-to-energy facilities, metallurgical smelting exhaust, and battery fire barriers, maintaining physical integrity up to 260°C continuous exposure with inherent flame retardance (LOI > 28%).
Technical Roadmap
Fiber Matrices & Mechanical Specifications
Quantitative property metrics across our core hydroentangled product spectrum to simplify technical qualification and procurement screening.
| Matrix Composition | Basis Weight Range | Tensile Strength (MD/CD) | Elongation at Break | Primary Industrial Utility |
|---|---|---|---|---|
| 100% Virgin Viscose | 35 – 120 gsm | ≥ 75 / 55 N/5cm | 25% / 65% | Biodegradable beauty masks, flushable wipes, medical dressings |
| 70% PET / 30% Viscose Blend | 40 – 160 gsm | ≥ 110 / 85 N/5cm | 35% / 70% | Heavy-duty industrial wiping, hygiene, wet-wipe base sheets |
| 100% rPET (Recycled Poly) | 45 – 220 gsm | ≥ 130 / 115 N/5cm | 40% / 60% | Eco-conscious synthetic leather base, acoustic backing, lining |
| 100% Polypropylene (PP) | 30 – 100 gsm | ≥ 95 / 80 N/5cm | 45% / 75% | Chemical-resistant wipers, oil-absorbent pads, battery separators |
| Specialty (PI / Basalt / Pre-Ox) | 80 – 350 gsm | ≥ 240 / 210 N/5cm | 15% / 25% | Thermal insulation, thermal runaway wraps, high-temp baghouses |
Supply Chain Excellence
Integrated Manufacturing Infrastructure in Changshu, Jiangsu
A vertically unified operational framework that consolidates fiber preparation, hydroentanglement, chemical treatment, and QA under one roof.
Single-Site Vertical Integration
Traditional nonwovens supply chains involve multiple subcontractors: one for base fabric carding, another for batch dyeing, and a third for functional finishing. YDL Nonwovens eliminates this fragmented model by managing raw polymer blending, hydroentangling, sizing, disperse/reactive dyeing, and precision slitting inside our Changshu manufacturing facility. This integrated setup reduces conversion cycle times by 35% and maintains uniform quality across high-volume production runs.
Petrochemical & Fiber Proximity
Located in the heart of China’s textile manufacturing belt in Jiangsu Province, our mill maintains upstream raw material pipelines with major global polyester and viscose staple producers. This geographic proximity minimizes freight costs, provides buffer stock resilience against commodity polymer price spikes, and guarantees uninterrupted production during periods of global logistics volatility.
Logistics & Deep-Water Export Routing
Our proximity to Shanghai and Ningbo deep-water ports provides reliable container staging and daily drayage options. Supported by our experienced export documentation team, international shipments benefit from clear customs processing, optimized roll palletization to maximize TEU container load factors, and verified compliance with EU, North American, and APAC entry standards.
Audited Quality Assurance
Global Compliance & Laboratory Verification
Stringent multi-stage inspection procedures from raw bale opening to optical defect scanning of finished slit master rolls.
ISO 9001 Process Discipline
Every operational lot adheres to strict digital standard operating procedures. In-line gamma gauges monitor areal weight uniformity in real time across the complete web width. Our in-house quality assurance laboratory verifies tensile parameters, tear strength, liquid strike-through, and residual fiber extractables for every production run, with lot samples archived for 24 months.
Chemical & Regulatory Safety
Functional chemistries and auxiliary agents undergo thorough toxicological screenings. Our materials comply with REACH (EC 1907/2006) and RoHS limits, contain zero SVHCs (Substances of Very High Concern), and are manufactured free of alkylphenol ethoxylates (APEO) or intentionally added PFAS, meeting target safety standards for skin contact and eco-sensitive end uses.
Fibershed Traceability & ESG
To support global corporate ESG and zero-deforestation mandates, our cellulosic viscose staple fibers are sourced exclusively from Chain of Custody certified wood pulp suppliers. For circular economy projects, our rPET offerings incorporate recycled consumer bottle flake resin traceable to Global Recycled Standard (GRS) baseline documentation.
Specialized Finishing & Technical Formulations
High-Specification Substrates & Functional Finishes
Purpose-engineered nonwovens delivering flame protection, color transformation, structural stiffening, and custom decorative performance.
Full-Cross Lapped Ultra-Uniform Spunlace
Product Specifications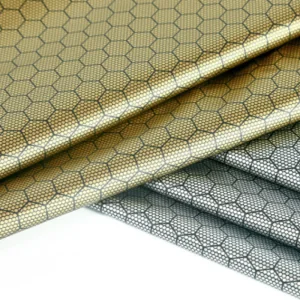
Gold & Silver Stamped Decorative Spunlace
Product Specifications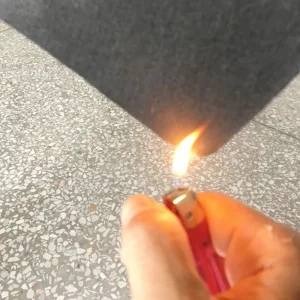
Flame Retardant Chemical Treated Spunlace
Product Specifications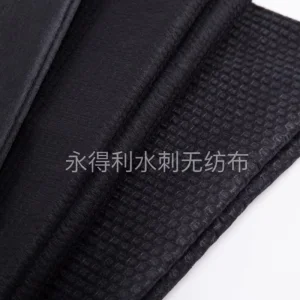
Jet-Black Pigmented Viscose Mask Matrix
Product Specifications
Low-Density Polypropylene (PP) Spunlace
Product Specifications
Photosensitive Color-Changing Smart Fabric
Product Specifications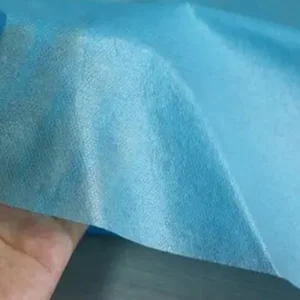
Extrusion Thermal Laminated Spunlace
Product Specifications
Powder-Dusted Hot-Melt Interlining Base
Product Specifications
Technical & Sourcing FAQ
Engineering Inquiries & Qualification Support
Direct technical answers addressing physical web properties, custom converting capabilities, and supplier onboarding parameters.
What are the primary differences between parallel-lapped and cross-lapped spunlace nonwovens?
The core difference lies in the fiber orientation during web formation. Parallel-lapped spunlace aligns staple fibers primarily along the Machine Direction (MD), providing high tensile strength along the roll length, but lower Cross-Direction (CD) strength (often a 4:1 ratio). This structure works well for basic wipes and straight converting applications. Cross-lapped webs overlap layers diagonally, balancing the fiber distribution to achieve an isotropic MD:CD ratio close to 1.2:1. This balance prevents neck-in narrowing under lamination tension and delivers uniform resistance against multi-directional stress.
How do you maintain lot-to-lot color accuracy in dyed and sized spunlace substrates?
Because our chemical treatment, continuous dip-pad sizing, and hot-air stenter operations run directly on-site, color match reproducibility is controlled by computerized dye dosing kitchens. We verify color parameters using standard spectrophotometers (evaluating Delta E under D65, TL84, and A light sources). Every batch is calibrated against an established physical master sample, maintaining a Delta E < 0.8 across repeat production orders to ensure seamless color matching for PU leather convertors.
What functional surface treatments can be integrated directly during primary processing?
Our integrated downstream finishing lines can apply a wide range of chemical formulations, including fluorocarbon-free hydrophobic finishes, durable hydrophilic surfactants, organophosphate flame retardants, static-dissipative antistatic coatings, cosmetic micro-encapsulations, and antimicrobial agents (such as silver ion or quaternary ammonium complexes). Applying these treatments in-line ensures chemical penetration through the entire fiber network rather than just topical surface deposition.
What testing documentation and Quality Certificates are provided with industrial roll shipments?
Every shipment roll is labeled with an individual barcode for traceability back to raw staple bale numbers and operational shifts. Shipments include a standard Certificate of Analysis (COA) containing verified laboratory testing data: basis weight verification (ISO 9073-1), tensile strength and elongation metrics (ISO 9073-3), liquid absorbency capacity (ISO 9073-6), and thickness under controlled load. REACH, RoHS, and biocompatibility documentation can be supplied for compliance screening upon request.
What minimum production quantities (MOQ) and packaging formats apply to specialized export orders?
Standard white conventional spunlace runs require a minimum order volume of 1,000 kg for regular production lots. Custom dope-dyed, pigment-printed, or chemical-functionalized webs require an MOQ of 3,000 kg depending on specific basis weight parameters. Rolls are wound on reinforced 3-inch or 6-inch inner cardboard cores, sealed in heavy-duty polyethylene barrier film against moisture intrusion, wrapped in woven polypropylene jackets, and palletized for export loading.