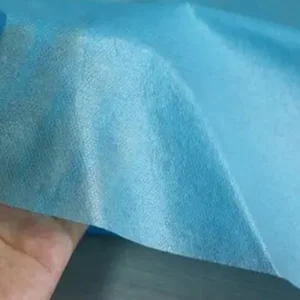
Film Laminated Spunlace for Boston MedTech Drapes & Isolation
- Structure: Spunlace + Breathable PE/PU Film
- Weight: 45 – 110 GSM
- Target: AAMI Level 3/4 Surgical Barrier
Direct from our precision manufacturing facility: Engineered spunlace configurations optimized for medical gowning, critical microelectronics, cleanrooms, and thermal insulation.
The Greater Boston metropolitan area—anchored by Cambridge's Kendall Square, the Route 128 tech expressway, and the I-495 biomanufacturing beltway—represents North America’s most concentrated cluster of life sciences, biomedical device fabrication, high-tier pharmaceuticals, and precision microelectronics. For procurement leaders and process engineers operating across Middlesex, Norfolk, and Suffolk counties, nonwoven materials are not mundane commodities; they are mission-critical consumables that directly dictate cleanroom yield, regulatory compliance, and patient safety.
Traditional nonwovens frequently fail under the rigorous standards mandated by FDA-regulated medical packaging converters in MetroWest or cleanroom wiper distributors serving semiconductor research labs around Waltham and Lexington. Conventional spunlace—manufactured via high-energy hydroentanglement without chemical resin binders—delivers the low-particulate, lint-free, and hyper-absorbent profile demanded by these technical sectors.
Regional research and manufacturing output requires zero-defect hydroentangled substrates with verified lot traceability.
Procuring spunlace for the Boston market requires bridging technical precision with extreme supply chain resilience. Here is how YDL Nonwovens delivers superior value from our Changshu, Jiangsu deep-water manufacturing hub.
Unlike regional US converters who buy base fabrics, broker dyeing, and outsource chemical finishing to third parties—introducing cross-contamination and markups—our facility executes virgin fiber opening, high-pressure carding, hydroentanglement, continuous dyeing, sizing, and functional finishing inside one ISO 9001 facility.
Our multi-stage deionized water needle injectors operate at hydraulic pressures up to 250 bar. By adjusting specific hydraulic energy per unit mass, we precisely calibrate fiber entanglement density, achieving high bulk softness while eliminating loose fiber shed to satisfy strict Cambridge biopharma standards.
Every meter of spunlace web is monitored by multi-camera optical inspection systems detecting defects, black specs, oil drop spots, and edge thickness variations down to 0.3mm. Batch testing includes tensile MD/CD elongation, water/solvent absorption capacity, surface resistivity, and bio-burden counts.
Driven by European sustainability directives and aggressive Massachusetts state environmental policies, nonwoven procurement is undergoing a generational shift from synthetic fossils to bio-based and functional polymers.
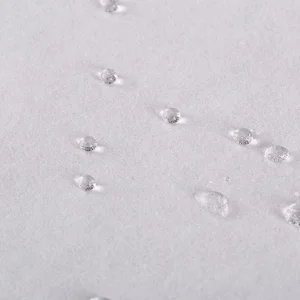
The nonwovens sector in the northeastern United States faces strict regulatory scrutiny. The Massachusetts Department of Environmental Protection (MassDEP) and federal regulatory bodies are aggressively monitoring poly- and perfluoroalkyl substances (PFAS) commonly used in nonwoven barrier coatings. In response, YDL Nonwovens has pioneered advanced fluorine-free water repellency (DWR) and mechanical liquid barrier technologies that achieve outstanding hydrostatic head pressure without chemical bio-accumulation.
Concurrently, corporate sustainability mandates in Boston’s corporate procurement suites are driving the transition toward completely plastic-free hygiene and industrial wipe substrates. Our production lines seamlessly run 100% FSC-certified viscose, bamboo fiber, and pure Polylactic Acid (PLA) polymers derived from renewable agricultural resources. These biodegradable hydroentangled fabrics achieve equivalent tensile strength and superior fluid absorbency compared to virgin PET, fully degrading under standard industrial composting conditions without leaving microplastic residues.
How our conventional and engineered functional spunlace webs integrate into local industrial converting workflows throughout New England.
Use Case: Surgical prep pads, orthopedic cast padding, wound contact layers, and patient draping.
Key Spec: 40–80 GSM apertured or plain PET/Viscose blends. Non-cytotoxic, hypoallergenic, gamma/EtO sterilization compatible, with instantaneous water pick-up exceeding 800% dry weight.
Use Case: Cleanroom wipedown in Andover, North Reading, and Marlborough semiconductor/laser testing facilities.
Key Spec: 55–70 GSM 55% cellulose / 45% polyester hydroentangled blend. Low ionic contamination (chloride, sodium < 5 ppm), abrasion-resistant, and solvent compatible.
Use Case: Backing cloth for high-end synthetic upholstery, boat seating, and institutional contract furniture.
Key Spec: 80–220 GSM dyed and stiffness-sized spunlace. Balanced cross-lapping web structure that prevents surface orange peel during polyurethane coagulation.
Comprehensive physical properties comparing standard spunlace configurations against advanced functional variations engineered by YDL Nonwovens.
| Substrate Category | Fiber Blend Ratio | Basis Weight (GSM) | MD/CD Tensile (N/5cm) | Absorbency Capacity | Compliance & Certs |
|---|---|---|---|---|---|
| Conventional Plain White | 70% Polyester / 30% Viscose | 40 – 65 g/m² | ≥ 120 / ≥ 95 | 750% – 850% | ISO 9001, OEKO-TEX 100 |
| Medical Grade Apertured | 50% Viscose / 50% Polyester | 45 – 80 g/m² | ≥ 140 / ≥ 110 | > 900% (Instant) | USP Class VI, Cytotoxicity |
| Cleanroom Critical Blend | 55% Woodpulp / 45% PET | 55 – 68 g/m² | ≥ 160 / ≥ 80 | 600% – 700% | IEST-RP-CC004.3 Clean |
| Dyed Synthetic Leather Base | 100% Micro PET (Cross-lapped) | 90 – 220 g/m² | ≥ 320 / ≥ 290 | Coating Substrate | REACH, RoHS, Anti-Delam |
| Flame Retardant Functional | Pre-Oxidized / Viscose FR | 120 – 350 g/m² | ≥ 280 / ≥ 240 | Thermal Shield | NFPA 701, FAR 25.853 |
Need a custom slit width, specific reel outer diameter (OD), or proprietary resin impregnation finish?
Request Custom Lab Samples & Master RollsExplore our full technological suite of surface-modified, extrusion-laminated, and high-temperature technical hydroentangled fabrics available for immediate export to Boston (Conley Terminal) and New York ports.
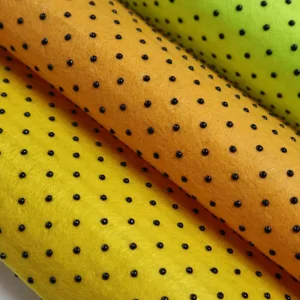
Key commercial, logistical, and technical considerations for procurement executives evaluating direct mill partnership with YDL Nonwovens.
Production cycles typically run 15–20 working days depending on customization (slitting widths, dyeing, sizing). Ocean transit from Shanghai/Taicang to Conley Terminal in Boston or the Port of New York/New Jersey averages 28 to 35 days on standard liner services. We offer complete DDP, CIF, or FOB terms with all US customs documentation and ISF filings managed smoothly.
Spunlace achieves bonding purely via pressurized water jets, preserving fiber softness without stiffening resins or molten plastic nodules. Compared to needlepunch, spunlace is much lighter (down to 30 GSM) and exhibits drastically superior surface uniformity, higher liquid pick-up capacity, and zero chemical leachables, making it superior for clinical and cleanroom wiping.
Yes. All functional liquid repellent treatments can be formulated 100% fluorine-free to comply with Massachusetts state environmental regulations. Furthermore, our 100% Viscose, Bamboo, and PLA spunlace substrates carry full biodegradability certifications and comply with European EN 13432 and ASTM D6400 commercial composting criteria.
For standard white conventional spunlace (plain, mesh, or embossed), our standard MOQ is 1,000 kg per specification. For custom reactive dyeing, color matching, special sizing stiffness, or high-performance chemical treatments, the baseline MOQ is 2,000–3,000 kg. We regularly support OEM trial runs with lower-quantity pilot rolls for lab verification and prototyping.
High-speed converting machinery requires dimensional stability under tension. Our production lines utilize computerized cross-lapping and balanced drafting units rather than simple parallel carding. This allows us to calibrate the MD:CD tensile ratio down to 1.1:1, preventing web neck-in, stretching, or tear out during high-speed medical slitting or synthetic leather laminating.
Every commercial lot is dispatched with an ISO 9001 certified Certificate of Analysis (COA) specifying tested basis weight, thickness, tensile strength (MD and CD), elongation curves, water/oil absorption capacity, bioburden/cleanliness metrics, and moisture levels measured across beginning, middle, and end roll samples.