Featured High-Performance Substrates
Direct supply line selections for specialized medical conversion, sterile protective barriers, and high-tensile hydroentangled platforms.
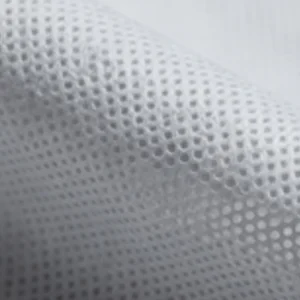
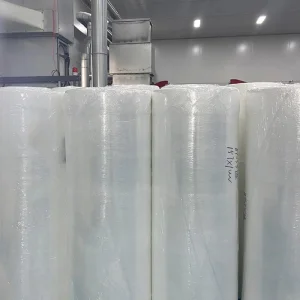
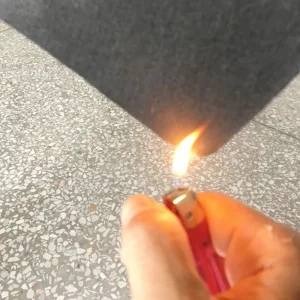
The Architecture of PE Film Coated Laminated PP Nonwovens
Decoupling the mechanical matrix and fluid barrier: How composite extrusion lamination yields impermeable, lint-free protection for medical class I-IV settings.
Impermeable Film Synthesis
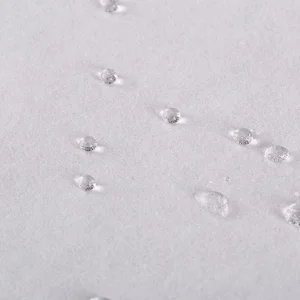
Polyethylene (PE) coating delivers a monolithic liquid barrier, ensuring total resistance against bloodborne pathogens, cellular exudates, and aggressive chemical disinfectants without pinhole compromises.
Spunbond Structural Rigidity
The Polypropylene (PP) core fabric supplies balanced longitudinal (MD) and transversal (CD) tensile elasticity, tear resistance under dynamic movement, and stable tactile ergonomics for surgical teams.
Microporous Breathability
Advanced microporous modifications permit moisture vapor transmission (MVTR > 3000 g/m²/24hr) while completely halting aqueous ingress, dramatically mitigating heat fatigue during prolonged surgical interventions.
Global Procurement Demands & Industry Trends
Navigating the shift toward composite PPE materials, regulatory sterilization compliance, and circular healthcare supply dynamics.
AAMI Level 3 & 4 Transition
Tier-1 hospital chains are standardizing purchasing specifications toward laminated barriers that pass ASTM F1670 (synthetic blood) and ASTM F1671 (viral penetration) for high-fluid orthopedic and cardiovascular theaters.
Sterilization Neutrality
Global procurement requires materials formulated to retain dimensional stability and tensile strength under Gamma radiation, Ethylene Oxide (EtO), and low-temperature E-beam terminal sterilization modalities.
Polyolefin Recyclability
Because both the carrier nonwoven (PP) and the lamination film (PE) are polyolefins, downstream hospital waste systems can recycle compatible streams, minimizing incineration footprint compared to multi-resin matrices.
China Factory 4.0: Manufacturing Resilience & Quality Scalability
Integrating high-speed extrusion lines with machine vision inspection to achieve absolute consistency across high-volume industrial consignments.
Vertical Pellet-to-Roll Mills
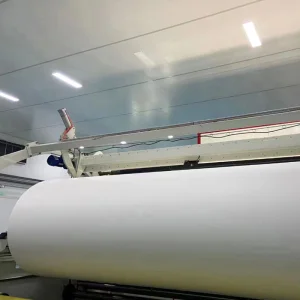
By producing base nonwovens and operating in-line cast film extrusion lamination on continuous corridors, Chinese facilities minimize transport oxidation, particulate ingress, and intermediate handling charges.
Optical Pin-Hole Inspection
Integrated CCD machine vision scanners sweep 100% of the unwound web at line speeds of 400 m/min, tagging and eliminating micro-voids, thickness variances, and gel contaminations down to 0.1 mm precision.
Dynamic Resin Hedging
Close proximity to Sinopec and global virgin polymer sources affords real-time hedging against global PP/PE commodity price swings, offering stable long-term volume contracts for medical brands.
ISO 13485 Cleanroom Facilities
All finished slitting, core inspection, and vacuum-sealed bagging occur inside climate-controlled clean environments, avoiding particulate contamination for sterile device converting suites.
Substrate Engineering Matrix: Standard vs. PE Laminated
A side-by-side engineering evaluation between standard spunbond substrates, SMS barriers, and PE film extrusion coated PP laminates.
| Performance Parameter | Standard Spunbond (PP) | SMS Multilayer Composite | PE Coated Laminated PP Nonwoven |
|---|---|---|---|
| Hydrostatic Head (AATCC 127) | < 20 cm H2O (Basic splash) | 50 - 85 cm H2O (Medium barrier) | > 200 cm H2O (Absolute Fluid Barrier) |
| Viral Penetration (ASTM F1671) | Fails under light pressure | Conditional (GSM dependent) | Pass (Zero Penetration Guaranteed) |
| Lint Generation (Gelbbo Flex) | Low to Medium | Very Low | Zero Lint (PE Barrier Sealed) |
| Surface Tensile Strength (MD/CD) | Moderate (35-65 N/5cm) | Strong (60-95 N/5cm) | Reinforced Elasticity (> 110 N/5cm) |
| Target Classification | AAMI Level 1 (General Isolation) | AAMI Level 2-3 (Standard Gowns) | AAMI Level 4 (Critical Surgical Zones) |
Deployment Across Localized Industrial & Healthcare Scenarios
Specific converting workflows relying on thermal laminated and hydroentangled synthetic matrices.
Critical Zone Surgical Drapes
Reinforcing the incision site fenestration with impermeable PE film coated laminated PP to eliminate fluid migration and strike-through contamination during major orthopedic procedures.
Biological Protection Coveralls
Engineered for biosafety Level 3 and 4 containment uniforms, ultrasonic sealed seam tape adhesion, and resistance to pressurized sprays during hazardous emergency sanitization sweeps.
Mortuary & Autopsy Protective Gear
Complete hydrophobic containment matrices ensuring high physical puncture resistance and comprehensive airborne pathogen separation for medical examiner teams and pathologists.
Frequently Asked Questions (Sourcing & Engineering)
Expert answers addressing the qualification, inspection, and delivery criteria of PE laminated medical nonwovens.
What makes PE laminated PP nonwoven superior to traditional SMS for AAMI Level 4?
While SMS fabrics utilize meltblown filament networks that rely on fiber density to resist liquid, sufficiently pressurized fluid will eventually penetrate. PE film extrusion creates a continuous, pore-free monolithic membrane that stops 100% of fluids and micro-pathogens, satisfying ASTM F1670 and F1671 standards.
Can the PE coating be adjusted for both breathable and non-breathable requirements?
Yes. Extrusion can utilize solid virgin LDPE/LLDPE for complete fluid locks, or cast microporous films impregnated with calcium carbonate (CaCO3) fillers, which are stretched during fabrication to generate tortuous paths for air and vapor while retaining high hydrostatic resistance.
How do you verify roll lamination peel strength?
Bond strength is validated via universal tensile test benches according to ASTM D2724 or ISO 2411. We guarantee high inter-ply adhesion (> 2.5 N/25mm) preventing delamination during cutting, sewing, high-frequency sonic welding, or vigorous surgical manipulation.
What are the standard MOQ, lead time, and core packing options for export?
Standard export production rounds run on an MOQ of 2 metric tons per specification. Lead time spans 10 to 18 operational days from resin staging. Rolls are supplied on 3-inch reinforced paper cores wrapped with high-micron PE stretch film and sealed edge guards for oceanic transport.
Engineered Functional Nonwoven Portfolio
Complete your supply specification with specialized treatments, electro-active layers, and antimicrobial performance fibers.
Schedule an Engineering Sample Run
Connect with our technical division to receive slit coil swatches, ISO 10993 cytotoxicity documentation, and direct mill quotes.