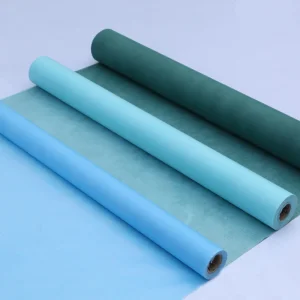
Featured Precision Spunlace & Functional Material Roster
High-integrity nonwoven materials tailored for clinical hygiene, composite matrices, electrostatic separation, and high-temp industrial environments.
Global Nonwoven PET Dynamics, Molecular Engineering & Industrial Reality
Technical appraisal of Polyethylene Terephthalate (PET) in spunlace hydroentanglement matrices and technical substrate manufacturing.
Global Polymer Market Position
Polyethylene Terephthalate (PET) remains the bedrock of structural nonwovens due to its superior glass transition threshold (approx. 78°C) and melting spectrum between 250°C and 260°C. Compared to Polypropylene (PP), PET maintains high dimensional integrity under thermal strain, superior tensile performance, and intrinsic receptivity to reactive dispersion colorants and customized chemical formulations.
Sustainability & rPET Imperatives
Global corporate procurement directives demand elevated integration of post-consumer recycled PET (rPET). Mechanically and chemically recycled filament and staple fiber lines require exact fiber crimp uniformity and oil-agent management to withstand severe high-pressure hydraulic needle impacts (up to 200 bar) without fiber breakage or particulate shedding.
High-Efficiency Vertical Processing
Integrated production plants circumventing external processing minimize lot-to-lot coefficient of variation (CV%). At YDL Nonwovens (Changshu Yongdeli), fiber preparation, carding, cross-lapping, hydroentanglement bonding, continuous drying, thermofixation, and chemical sizing occur within a singular, ISO 9001 certified closed ecosystem.
Localized Application Scenarios & Engineering Specifications
From automotive cabin linings to clinical infection barriers, nonwoven PET structures are parameterized to exact mechanical parameters.
Synthetic Leather Reinforcement
Microfiber synthetic leather formulations and high-grade polyurethane (PU) skin substrates demand balanced Machine Direction (MD) to Cross Direction (CD) tensile ratios (approximating 1:1 via cross-lapping). Calendered and sized PET hydroentangled webs prevent delamination under deep thermal molding cycles in automotive seating and high-flex luxury footwear.
Medical & Surgical Protective Media
Engineered hydroentangled webs combining PET with wood pulp or viscose deliver high liquid strike-through resistance, static dissipation, and alcohol repellency. Binder-free jet entanglement guarantees that no synthetic chemical residuals leach upon sterilizing irradiation (gamma or EO gas), meeting AAMI Level 3 and 4 surgical barrier standards.
High-Efficiency Air & Liquid Filtration
PET matrices provide superior structural stiffness over polypropylene in pleated filter configurations. Functionalized via electrostatic charging, triboelectric treatment, or nano-graphene compounding, PET substrates capture micro-particulates with minimal differential pressure loss across HVAC, industrial baghouses, and coolant filtration lines.
| Application Category | Base Polymer Blend | Hydroentanglement Density (GSM) | Mechanical / Functional Attribute | Target Metric |
|---|---|---|---|---|
| Automotive Interior / PU Leather | 100% Sized PET / Micro-PET | 80 - 220 GSM | Low Thermal Shrinkage, High Peeling Strength | MD/CD Ratio ≤ 1.15; Shrinkage < 1% at 150°C |
| Aseptic Medical Barriers | PET / Viscose / Cellulose | 45 - 80 GSM | Hydrostatic Head, Alcohol/Blood Repellency | AATCC 127 ≥ 50 cm H2O; Zero Binder Extraction |
| Industrial Dust & Gas Filtration | High-Tenacity PET / Polyimide (PI) | 100 - 400 GSM | Continuous Heat & Chemical Resistance | Air Permeability: 100-300 L/m²/s @ 200Pa; Temp to 150°C |
| Laundry Color Absorption Sheets | Modified Viscose / PET Matrix | 50 - 75 GSM | Cationic Quaternary Dye Scavenging | Direct Red/Blue Dye Fixation > 98.5% |
| Structural Fire Barriers | Pre-Oxidized Fiber / Basalt / PET | 120 - 350 GSM | Flame Arrestance, Zero Molten Droplet | LOI ≥ 32%; UL94 V-0 Certified Performance |
Technological Roadmap: 2026–2030 Precision Outlook
Architecting next-generation nonwoven hydroentanglement through surface nanocoating, inline optical telemetry, and circular polymer regeneration.
Phase 1: Ultrafine Hydro-Splitting
Optimizing bicomponent (islands-in-the-sea / segmented pie) PET/PA6 fibers. By implementing ultra-high pressure water manifolds (250+ bar), fibers dissociate into micro-filaments below 0.05 dtex, unlocking surgical barrier performance without chemical adhesives.
Phase 2: In-Line AI Spectral Surface Analysis
Deploying continuous hyperspectral vision systems over high-speed winders. Neural net detection engines identify micro-nep anomalies, aperture distortions, and surface tension variations down to 0.1mm at web transit speeds exceeding 250 m/min.
Phase 3: Deep Green Molecular Circularity
Achieving zero-carbon footprint web manufacturing by coupling chemically recycled bio-PET with biodegradable PHA/PLA hybrid networks, validated through real-time Lifecycle Carbon Assessment (LCA) tracking protocols.
Macro-Industry Procurement & Operational Solutions
Mitigating systemic bottlenecks across international nonwoven roll-goods distribution and manufacturing pipelines.
Lot Consistency Mitigation
Fragmented supply chains cause variable tensile modulus and differential shrinkage. YDL eliminates vendor divergence by synthesizing raw fiber opening, high-velocity hydroentanglement, coloration, and topical sizing inside a single Changshu facility under an ISO 9001 certified regime.
Low-Fiber Shedding Assurance
Standard spunlace grades can release lint under vigorous wiping or coating sheer. Our multi-stage vacuum dewatering and pressurized hydraulic needle configuration locks superficial staple ends into the interior core, maintaining Class 100 cleanroom compliance.
Tariff & Freight Optimization
Bulky roll-goods create exorbitant sea shipping costs. Through calibrated roll compaction, continuous tension rewinding, and optimized core dimensions, YDL increases container volumetric cargo efficiency by 18-24%, reducing shipping costs per square meter.
Regulatory Compliance Safeguards
We run extensive lab verification for compliance with EU REACH (SVHC), RoHS, OEKO-TEX Standard 100, and FDA food-contact mandates. Our chemistry completely excludes fluorinated organics (PFAS/PFOA) in standard water-repellent finishing runs.
Frequently Asked Questions (Technical Sourcing FAQ)
Direct answers to core specifications, processing tolerances, and compliance requirements for nonwoven PET buyers.
What fundamental differences exist between PET and Polypropylene (PP) nonwovens?
How does YDL ensure strict Machine Direction (MD) and Cross Direction (CD) balance?
Can you provide hydrophobic, oleophobic, or flame-retardant (FR) treatments in-house?
What is the standard production lead time and roll customization capability?
Advanced Substrate & Specialized Nonwoven Range
High-performance technical fabrics engineered for electrical conductivity, specialized filtration, and thermal insulation.