Engineered Fabric Solutions: Featured Showcase (Part I)
Explore our baseline and specialty high-loft, embossed, and functional nonwoven rolls tailored for medical, hygiene, filtration, and precision industrial applications.
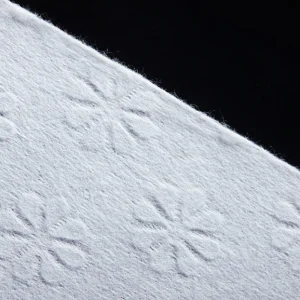
High-Quality Embossed Nonwoven Fabric
Explore Product Specifications
Anti-Mite Spunlace Nonwoven Fabric
Explore Product Specifications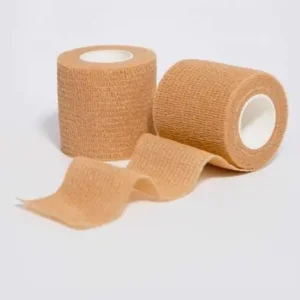
Spandex Elastic Spunlace Nonwoven
Explore Product Specifications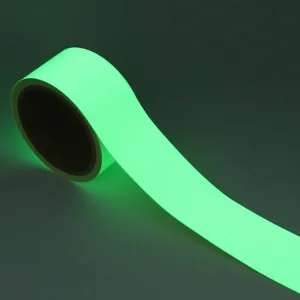
China Noctilucent Nonwoven Fabric
Explore Product Specifications
Extrusion Laminated Nonwoven Substrates
Explore Product Specifications
Recycled Polyester (rPET) Nonwoven
Explore Product Specifications
Full-Cross Balanced Nonwoven Web
Explore Product Specifications
Polypropylene (PP) Technical Nonwoven
Explore Product SpecificationsThe Engineering Science of Hot-Air Nonwoven (Through-Air Bonding)
Hot-Air Through-Bonded Nonwoven (frequently designated as ATB or Air-Through Nonwoven) represents a pinnacle class of high-bulk, ultra-soft technical textiles engineered primarily via bicomponent staple filaments. In contrast to spunlace (hydroentanglement), which interlocks fibers mechanically utilizing supersonic hydraulic water needles, or calender thermal bonding, which consolidates web sheets via direct compressive mechanical rollers, hot-air through bonding relies exclusively on controlled thermodynamic convective air currents.
The carded web passes smoothly over an insulated, perforated suction drum or horizontal conveyor oven. Heated air at tightly calibrated temperatures passes perpendicularly through the uncompressed fiber batting. Bicomponent staple fibers—typically sporting an ES (Ethylene-Propylene side-by-side or Polyethylene/Polypropylene sheath-core morphology)—fuse solely at the outer low-melting sheath (PE ~130°C), while the inner high-melting core (PET or PP ~165°C–260°C) retains absolute structural integrity.
Information Gain Insight: Because the consolidation eliminates mechanical compression rollers, the individual polymer loops maintain a lofty, open three-dimensional skeletal matrix. This guarantees pore volume exceeding 85%, conferring near-instantaneous fluid acquisition velocities, minimal rewet percentages (<0.05g), and a feather-soft sensory coefficient crucial for delicate dermis interfaces.
Consequently, through-air bonded substrates deliver an unmatched recovery rate under compressive loads, positioning them as the indispensable baseline for high-tier absorbent hygiene products (AHP), premium adult incontinence topsheets, and high-efficiency pre-filtration particulate barriers.
Dermal Micro-Climate Regulation
The open-cell geometry of air-through fabrics facilitates continuous thermal exchange and moisture vapor dissipation. Clinical trials substantiate that replacing calendered spunbond with hot-air nonwoven decreases cutaneous relative humidity by up to 24%, dramatically reducing the etiology of diaper dermatitis and friction rashes.
Z-Direction Fluid Dynamics
Unlike planar materials that exhibit lateral fluid migration, the orthogonal fiber alignment of air-through materials guides liquids strictly downwards in the Z-axis into the superabsorbent core (SAP matrix), accelerating strike-through while preventing perimeter leakage.
Strategic Manufacturing Advantages of Our Chinese Facilities
Operating from Changshu, Jiangsu—China's prime advanced textile synthesis corridor—our facilities unify petrochemical raw material access, precision line automation, and global export infrastructure.
Integrated Upstream Polymer Feedstock
Our strategic proximity to primary chemical polymerization giants (Sinopec, Hengli Petrochemical) ensures immediate batch-certified access to virgin PE/PP, PE/PET sheath-core bicomponent pellets, as well as traceable bio-based PLA resins. This eliminates intermediary markups and shields international procurement partners from raw material volatility.
German Trützschler & Reifenhäuser Lines
Equipped with state-of-the-art dual-doffer cross-lapping and balanced air-through bonding tunnels, our production lines achieve uniform basis weight distributions with a standard deviation (CV value) under 1.8%. Real-time infrared radiometric gauges verify web consistency across active widths up to 3.2 meters.
Class 100,000 Cleanroom & Vision QC
Hygiene substrates undergo rigorous production within fully enclosed Class 100,000 cleanroom environments. Automated continuous high-definition CCD vision systems inspect 100% of the moving web, flagging and isolating foreign fibers, pinholes, resin spots, and color variances as minor as 0.2mm².
Global Industry Trends & Next-Generation Nonwoven Innovation
Analyzing structural shifts across the hygiene, medical disposables, and technical air filtration sectors from a sustainability and biomaterials lens.
The 100% Biodegradable PLA/PHA Paradigm
In adherence to the EU Single-Use Plastics Directive (SUPD), our laboratory has perfected air-through thermal bonding using 100% poly-lactic acid (PLA) and polyhydroxyalkanoate (PHA) bicomponent filaments. These deliver complete industrial compostability within 180 days while retaining over 90% of the tensile strength of conventional fossil-derived polymers.
3D Micro-Perforation & Topographic Embossing
By synchronizing thermal bonding with synchronized micro-sculpting cylinders, we produce deep 3D funnel and honeycomb topologies. These conical apertures trap viscous fluids (such as menstrual secretions and soft infant stool) beneath the surface plane, guaranteeing continuous epidermal isolation.
Ultra-Low GSM High-Loft Matrices
Traditional thermal bonding required heavy basis weights (30–45 gsm) to achieve adequate structural loft. Our patented carding geometry allows our mill to engineer ultra-thin 16–20 gsm webs that preserve an astonishing 0.75mm thickness, reducing shipping container freight volume and end-user carbon emissions by over 28%.
Localized Application Scenarios: Macro Industry Solutions
Engineered to satisfy demanding thermal, mechanical, and dermatological parameters across international consumer and B2B sectors.
Baby Diaper Topsheets & ADL
Deployed as premier acquisition distribution layers (ADL) and cloud-soft topsheets. High pore volume eliminates instant flooding, transporting liquid rapidly to the absorbent core.
Feminine & Adult Incontinence
Combines silk-protein surface modifiers with bicomponent thermal webs. Inhibits bacterial proliferation, mitigates volatile amine odors, and stops damp back-flow.
Automotive Acoustic Barriers
Thermal-resistant bicomponent polyester webs utilized for cabin door trim backing, headliner sound-dampening, and engine cowl thermal insulation under extreme under-hood heat cycles.
HVAC & Medical Pre-Filtration
Serves as low-pressure-drop, high-dust-holding pre-filters in hospital HEPA arrays, automotive cabin air filters, and respirators, prolonging electrostatically charged meltblown lifespan.
Global Enterprise Procurement Specification Matrix
Standardized physical, hydrological, and chemical verification criteria adhered to across all production batches. Compliant with ISO 9001, EDANA, INDA, and OEKO-TEX Standard 100.
| Grade Category | Polymer Architecture | Basis Weight | Thickness (0.5 kPa) | Strike-Through (Liquid) | Rewet Metric | Tensile MD / CD | Primary Compliance |
|---|---|---|---|---|---|---|---|
| Hygiene Ultra-Soft | PE / PET Sheath-Core ES | 18 - 25 gsm | 0.70 - 0.95 mm | ≤ 1.2 seconds | ≤ 0.04 g | ≥ 18 N / ≥ 5 N | OEKO-TEX Class 1 |
| High-Flux ADL | PP / PE Bicomponent | 28 - 45 gsm | 1.10 - 1.60 mm | ≤ 0.9 seconds | ≤ 0.02 g | ≥ 32 N / ≥ 9 N | REACH / FDA CFR |
| Bio-Degradable PLA | 100% PLA Bicomponent | 22 - 35 gsm | 0.65 - 0.85 mm | ≤ 1.5 seconds | ≤ 0.06 g | ≥ 16 N / ≥ 4 N | EN 13432 Compost |
| Filtration Pre-Stage | Coarse PET / Co-PET | 50 - 120 gsm | 2.00 - 4.50 mm | Hydrophobic N/A | High Void Matrix | ≥ 65 N / ≥ 30 N | ASHRAE 52.2 / EN 779 |
| Embossed 3D Tactile | Hydrophilic ES + Silicone | 22 - 30 gsm | 0.85 - 1.25 mm | ≤ 1.1 seconds | ≤ 0.03 g | ≥ 22 N / ≥ 7 N | Skin Hypoallergenic |
* Custom slitting available from 45mm to 3200mm. Calibrated coil core diameter: 76mm (3 inches) or 152mm (6 inches). UV-sterilized shrink wrapping applied standard.
Comprehensive Hot-Air Nonwoven Procurement FAQ
In-depth responses resolving engineering qualifications, commercial volumes, testing methodologies, and international delivery protocols.
What fundamentally distinguishes hot-air (air-through) nonwoven from conventional spunlace and spunbond nonwovens?
What fiber compositions and denier ranges does your factory process for air-through bonding?
How does your production process maintain consistent basis weight (GSM) across wide webs?
Can you manufacture 3D embossed and perforated hot-air nonwoven rolls?
What testing protocols are executed prior to B2B batch release?
What is your minimum order quantity (MOQ) and lead time for custom formulations?
How do you ensure zero contamination during slitting and export transit?
Do your fabrics comply with REACH, FDA, and OEKO-TEX Standard 100 Class 1 certifications?
High-Performance Engineering Catalog: Featured Showcase (Part II)
Explore our specialized colored, functional sizing, flame-retardant, high-temperature aramid, polyimide, and polymer-laminated product lines.
Engineered Colored Fiber Nonwovens
Explore Product Specifications
High-Stiffness Sizing Nonwoven Fabric
Explore Product Specifications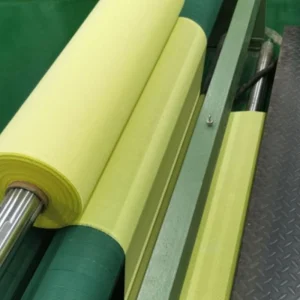
Thermal-Resistant Aramid Nonwoven
Explore Product Specifications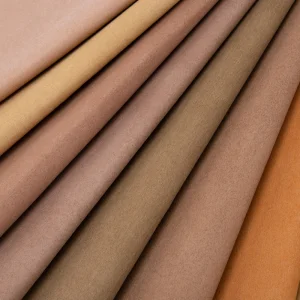
Off-Line Dyed Precision Nonwoven
Explore Product Specifications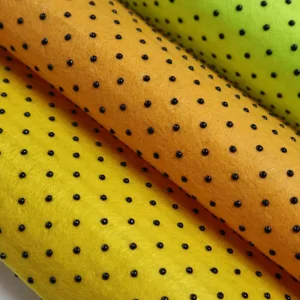
Anti-Slip Drop Plastic Nonwoven Web
Explore Product Specifications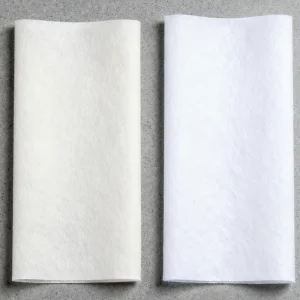
Optical Brightened Nonwoven Substrate
Explore Product Specifications
Polyimide (PI) Filtration Nonwoven
Explore Product Specifications