Engineered Medical & Functional Spunlace Lineup
Explore our core medical-grade and technical hydroentangled substrates, precision manufactured in Jiangsu for surgical drapes, wound dressings, protective gowns, and sensitive hygiene conversion.
Global Commercial Dynamics of Medical Nonwovens
Strategic analysis of clinical infection prevention requirements, standard shifts from woven to single-use hydroentangled textiles, and the modernization of Chinese manufacturing capabilities.
Clinical Mandates & Infection Control Protocols
The global healthcare arena has undergone a permanent structural transition following rigorous updates to infection control doctrines. Cross-contamination protocols mandated by the CDC, WHO, and European health authorities have accelerated the replacement of multi-use woven cotton linens with high-performance, single-use hydroentangled (spunlace) and composite nonwovens. Woven textiles shed microscopic fibers and degrade in hydrostatic barrier performance after multiple washing cycles. In contrast, precision-engineered spunlace nonwovens offer high tensile strength, consistent pore morphology, virtually zero linting, and impenetrable microbial barrier properties.
Stringent Regulatory Alignments (FDA, MDR, AAMI)
International procurement teams navigate increasingly complex regulatory landscapes. Medical nonwovens must strictly satisfy European Medical Device Regulation (EU MDR 2017/745), US FDA 510(k) clearance requirements, and the unified ANSI/AAMI PB70 liquid barrier standards. From AAMI Level 1 (minimal fluid exposure) up to AAMI Level 4 (viral penetration resistance under ASTM F1671), fabric suppliers in China must demonstrate total chemical purity, verifiable biocompatibility (ISO 10993 cytotoxicity and skin irritation protocols), and rigorous cleanroom processing to maintain an uninterrupted global commercial presence.
Procurement Trend Insight: Information Gain & Traceability
Modern tier-1 medical brands no longer evaluate nonwoven suppliers solely on cost-per-ton. The evaluation matrix has shifted toward **information gain, batch-to-batch coefficient of variation (CV% < 3%), automated optical defect classification**, and digital raw material traceability back to polymer synthesis. Chinese mills integrating in-house functional finishing are capturing global market share from fragmented secondary processors.
Clinical Application Scenarios & Fiber Formulations
How tailor-made hydroentangled architectures satisfy the divergent physical and chemical demands across operating rooms, intensive care units, and advanced wound management.
Surgical Gowns & O.R. Barrier Drapes
Operating theater barriers require an intricate balance between impervious fluid protection and long-duration ergonomic comfort. Utilizing cross-lapped spunlace blending 55% woodpulp/viscose with 45% polyester, treated with fluorochemical or fluorocarbon-free water/alcohol repellents, our drapes achieve AAMI Level 3 hydrostatic pressure resistance exceeding 50 cm H2O while maintaining exceptional breathability and soft drapeability that prevents glove contamination during surgical maneuvering.
Advanced Wound Care & Exudate Control
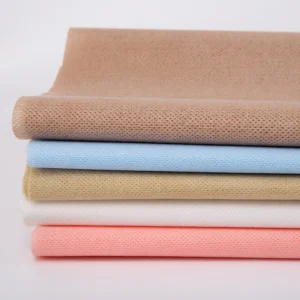
Chronic wound management demands specialized non-adherent contact surfaces and massive moisture retention. Our apertured (mesh) spunlace webs, composed of high-purity viscose and medical bamboo fibers, exhibit capillary absorption rates up to 900% of their base weight. Free of chemical binders, surfactants, or resin residues, these webs ensure zero mechanical tissue disruption during dressing changes and comply thoroughly with ISO 10993 cytotoxicity thresholds.
Sterile Barrier Packaging Systems
For terminally sterilized devices, barrier nonwovens must allow chemical sterilant penetrability (Ethylene Oxide or Gamma radiation) while establishing a tortuous, impenetrable microbial path against atmospheric spore reentry. Our specialized high-density SMS and dense-calendered PET spunlace formulations provide microbial barrier efficacy exceeding 99.98%, maintaining package sterility across five-year shelf-life stability validations under ASTM F1980 protocols.
Disinfection Converting & Antimicrobial Wipes
Surface contamination within clinical environments requires wipes engineered for quaternary ammonium (quat) compatibility. Standard cellulosic materials rapidly absorb cationic biocides, exhausting the active solution before surface application. We manufacture pure polypropylene and tailored synthetic spunlace matrices that release 100% of active biocidal formulations onto critical ICU surfaces without binder contamination or electrostatic cling.
Medical Tapes & Adhesive Dressings
Pressure-sensitive adhesive (PSA) tapes necessitate nonwoven carriers with high elongation recovery and balanced Machine Direction (MD) to Cross Direction (CD) tensile ratios. Our sizing spunlace and resin-free hydroentangled polyester backings provide uniform adhesive coatability, skin-conforming flexibility, and breathability that prevents epidermal maceration during multi-day patient fixation.
Filtration & Surgical Smoke Evacuation
Operating theater electrosurgical procedures produce carcinogenic plumes containing aerosolized cellular debris. We engineer multi-layered technical spunlace incorporating ultra-fine fiber blends and polyimide networks capable of serving as pre-filters and primary particulate traps, with minimal pressure drop (Delta P < 40 Pa) and high dust holding capacity under rigorous continuous clinical ventilation.
Chinese Supply Chain Resilience & Vertical Synergy
How the Changshu, Jiangsu industrial cluster pairs upstream polymer integration with in-house finishing to compress procurement lead times and eliminate subcontracting risks.
The Jiangsu Textile Belt: Raw Material Supremacy
YDL Nonwovens operates in Changshu, the global epicenter of nonwoven engineering and synthetic fiber technology in Jiangsu Province. This geographic proximity grants direct access to the world’s most advanced chemical fiber synthesis clusters, sourcing virgin polyester (PET), high-purity viscose, biodegradable PLA, and technical polymers from tier-1 petrochemical refineries within a 100-kilometer radius.
This hyper-localized raw material ecosystem buffers our manufacturing operations against global logistic bottlenecks, stabilizes bulk resin procurement pricing, and guarantees continuous raw staple fiber availability even during periods of extreme global supply disruption.
One-Roof Vertical Manufacturing Control
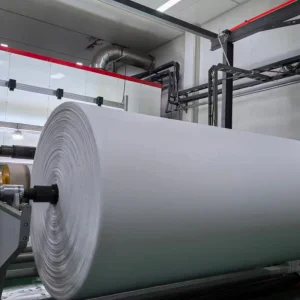
Unlike standard trading intermediaries or specialized convertors that outsource critical chemical processing, our facility houses comprehensive hydroentanglement, fiber blending, carding, cross-lapping, water recycling, pad-dyeing, chemical sizing, functional finishing, and automated high-speed slitting beneath one unified roof.
This single-roof model eliminates transit damage, controls cross-contamination, maintains lot-to-lot consistency through single-system digital QA tracking, and reduces production turnaround from industry averages of 45 days down to just 15–20 days for custom-specified medical grades.
Advanced Closed-Loop Water Recycling Infrastructure
Hydroentanglement demands billions of liters of high-purity water to power water needle jets operating at 60 to 180 bars of pressure. Our facility utilizes a multi-stage closed-loop automated biological and reverse osmosis (RO) filtration system, recovering over 92% of process water. This drastically decreases municipal fresh water consumption, insulates production from municipal water-use quotas, and guarantees mineral-free water quality that prevents salt crystallization or fiber staining during web formation.
Technology Roadmap & Sustainable Innovations (2025–2030)
Pioneering advancements across bio-degradable polymer chemistry, nano-structured surface modification, and artificial intelligence-guided quality inspection systems.
100% Bio-Circular Substrates
Full-scale commercialization of 100% biodegradable, compostable polylactic acid (PLA) and certified FSC/PEFC Lyocell spunlace. Formulated for complete marine and soil degradation without persistent microplastic accumulation, fulfilling strict European SUPD (Single-Use Plastics Directive) frameworks.
Fluorine-Free Barrier Chemistries
Elimination of long-chain PFAS/PFOA fluorochemicals. Deployment of novel bio-based dendrimer and nano-structured silane finishes delivering oil, blood, and alcohol repellency (AAMI Level 3/4) while maintaining clinical safety profiles and full environmental compliance with global chemical bans.
Functional Diagnostic Textiles
Integration of micro-encapsulated chromogenic and pH-sensitive reagents into hydroentangled matrices. Enables wound dressings to visibly alter coloration upon the onset of localized infection (alkaline shift), granting medical personnel instant diagnostic visual cues without dressing removal.
Electrospun Nano-Laminates
In-line hybrid hydroentanglement coupled with sub-micron electrospinning units. Creates ultra-dense nano-porous web filters with minimal air resistance (Delta P < 25 Pa) and viral filtration efficiency (VFE > 99.99%) for advanced biopharmaceutical sterile enclosures and life-support respirators.
Regulatory Compliance & Analytical Testing Matrix
Continuous verification protocols executed across cleanroom facilities to guarantee total lot-to-lot conformity with medical device manufacturing parameters.
| Evaluation Parameter | Reference International Standard | Certified Performance Threshold | Clinical Engineering Significance |
|---|---|---|---|
| Bacterial Barrier (BFE) | ASTM F2101 / EN 14683 | ≥ 99.5% Penetration Resistance | Prevents airborne pathogenic transmission across critical surgical theater barriers. |
| Liquid Barrier Rating | AATCC 42 / AATCC 127 | Hydrostatic Head > 50 cm H2O | Defines resistance against pressurized blood and bodily fluid spray during open surgical procedures. |
| Microbial Cleanliness | ISO 11737-1 | ≤ 10 CFU / 100g Fabric | Minimizes initial bioburden prior to terminal Gamma, ETO, or Steam sterilization cycles. |
| Lint Shedding / Gelbo | ISO 9073-10 / EN 13795 | Lint Factor Coefficient < 2.0 | Eliminates foreign particle contamination into open patient incisions during invasive surgery. |
| Biocompatibility Profile | ISO 10993-5, -10 | Zero Cytotoxicity & Zero Irritation | Guarantees chemical neutrality and skin safety for extended dermal contact wound dressings. |
| Tensile MD / CD Ratio | ISO 9073-3 | Ratio Balanced 1.1:1 to 1.4:1 | Prevents directional fabric tearing under high-speed automatic converting and surgical tension. |
Inline Laser Web Inspection
Every meter of fabric passes through 4K high-speed CCD line-scan camera systems, automatically flagging and categorizing pinholes, slubs, dark specks, or foreign fibers larger than 0.1 mm² with instant roll mapping.
Cleanroom Controlled Slitting
Finished master rolls are slit and converted in positive-pressure, dust-controlled cleanroom environments to maintain low bioburden thresholds and prevent particulate settling on sensitive medical web surfaces.
Full ERP Lot Traceability
Unique barcoded QR identification tags link finished rolls back to individual fiber supplier bale lot numbers, carding run parameters, hydroentanglement water pressures, and operator shifts for complete regulatory audit readiness.
Material Engineering Specification Matrix
Reference technical profiles designed to assist medical procurement engineers in configuring fiber ratios, basis weights, and surface textures for designated clinical devices.
| Substrate Code | Fiber Composition | Basis Weight (GSM) | Surface Texture | Key Performance Attribute | Primary Medical End-Use |
|---|---|---|---|---|---|
| MED-SPUN-MESH | 70% Viscose / 30% PET | 35 – 80 g/m² | 16 / 22 Mesh Apertured | Fast Capillary Drainage, Low Adhesion | Absorbent Sponges, Secondary Dressings |
| BAR-PET-PLAIN | 100% Virgin High-Tenacity PET | 40 – 120 g/m² | Solid Smooth Plain Web | High Hydrostatic Head, High Tensile | Reinforced Surgical Gowns, Tray Liners |
| ANTI-BAC-SILV | Blend with Silver/Chitosan | 45 – 90 g/m² | Pearl Embossed / Plain | >99.9% Antibacterial Efficacy | Antimicrobial Wipes, ICU Surface Disinfection |
| BIO-PLA-ECO | 100% Pure Corn Polylactide | 30 – 70 g/m² | Smooth / Micro-Apertured | 100% Biodegradable, Ocean Safe | Eco-Friendly Hygiene & Cleanroom Swabs |
| SIZE-POLY-STIFF | 100% Polyester with Sizing | 60 – 150 g/m² | Rigid Calendered Finish | Dimensional Stability, No Elongation | Medical Tapes, Plaster Backing Cloth |
| DOPE-DYE-SURG | 55% Cellulose / 45% PET | 50 – 75 g/m² | Medical Blue / Green Solid | Non-Reflective, Zero Color Bleed | Operating Room Fenestration Drapes |
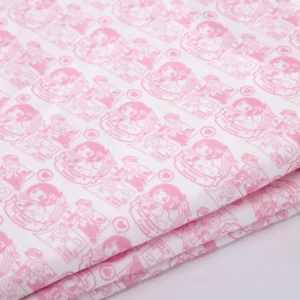
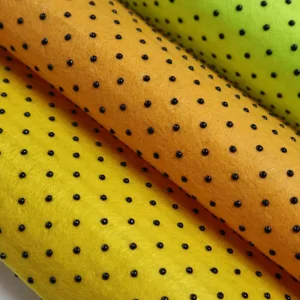
Specialized & High-Performance Roll Goods Lineup
Complete portfolio of functional, printing, synthetic leather backing, and extreme-barrier technical hydroentangled nonwoven roll goods for industrial and healthcare converters.
Global Engineering Support & OEM/ODM Partnership Process
A systematic four-tier collaboration lifecycle designed to transition novel medical nonwoven concepts into validated, high-volume production rolls smoothly and predictably.
01. Material Scoping
Joint engineering review defining basis weight (GSM), blend composition, target tensile MD/CD ratios, liquid absorption capacities, and specific clinical compliance benchmarks (AAMI 1–4, EN 13795).
02. Rapid Prototyping
Production of 50-meter pilot trial rolls on our dedicated pilot carding lines within 7 business days, providing clients with tangible materials for converter line runnability and lamination trials.
03. Lab Validation
Comprehensive third-party testing covering biological safety (ISO 10993 cytotoxicity), hydrostatic head resistance, microbial cleanliness, and autoclave/ETO aging stability tests with full documentation.
04. Scale Production
Ramping to full multi-ton container output with inline laser defect monitoring, precision customized reel slitting, desiccated moisture-barrier wrapping, and direct sea-freight dispatch from Shanghai ports.
Comprehensive Technical & Sourcing FAQ
In-depth responses to critical engineering, manufacturing qualification, and international supply chain inquiries posed by global procurement directors.
How does your medical spunlace fabric achieve high barrier performance without compromising breathability?
Our spunlace nonwovens achieve exceptional liquid barrier properties through a combination of high-density micro-fiber carding, precision hydroentanglement water pressure tuning (which creates an ultra-tortuous physical pathway that resists fluid breakthrough), and advanced fluorocarbon-free surface treatments. Because the hydroentanglement process bonds fibers mechanically without creating continuous, impermeable film skins (as in extruded films), microscopic interstitial air voids remain open. This architecture permits vapor transmission (breathability) while stopping high surface-tension liquids like saline and blood, easily meeting AAMI Level 2 and Level 3 liquid barrier thresholds.
What are your standard minimum order quantities (MOQ) and production turnaround timelines?
For standard conventional white spunlace nonwoven fabrics (PET, Viscose, or PET/Viscose standard blends), our standard commercial MOQ is 1,000 kg per specification. For custom-dyed, precision-printed, functional chemical finishes (e.g., antimicrobial, super water-repellent, or photosensitive), our MOQ is typically 2,000 kg to accommodate clean chemical bath charging. Standard lead times for containerized production orders range from 15 to 20 business days from technical specification sign-off, facilitated by our integrated in-house fiber inventory and rapid slitting infrastructure in Changshu.
Which sterilization methodologies are fully compatible with your medical nonwoven roll goods?
Our fabrics are engineered to withstand multiple sterilization protocols without structural degradation, tensile loss, or chemical breakdown. Our 100% polyester, polypropylene, and viscose-blend spunlace grades are fully compatible with Ethylene Oxide (ETO) sterilization, exhibiting rapid gas degassing profiles that prevent toxic residual buildup. For Gamma and E-beam radiation sterilization, we supply specialized radiation-stabilized polypropylene and high-tenacity PET that resist polymer chain scission and post-irradiation embrittlement. Furthermore, our high-temperature Polyimide and technical matrices tolerate autoclave steam sterilization at 121°C–134°C without shrinkage.
How do you maintain a low MD:CD tensile strength ratio, and why is this critical for medical converters?
Conventional parallel-laid spunlace often exhibits an unbalanced Machine Direction to Cross Direction (MD:CD) tensile ratio of 4:1 or 5:1, which can cause fabrics to narrow (necking), tear longitudinally, or stretch uncontrollably during high-speed automated web converting. At YDL Nonwovens, we utilize modern computer-controlled cross-lapping systems and multi-cylinder carding webs that cross-orient staple fibers prior to hydroentanglement. This balances our MD:CD ratio down to between 1.1:1 and 1.4:1, granting near-isotropic mechanical strength, zero web deformation under high web tension, and seamless running speeds exceeding 300 meters per minute on converting lines.
Can you provide technical data sheets (TDS), certificates of analysis (COA), and biological testing reports?
Yes. Every shipment is accompanied by a batch-specific Certificate of Analysis (COA) documenting actual basis weight, tensile properties (MD/CD breaking force and elongation), thickness, moisture regain, and bioburden limits. Full Technical Data Sheets (TDS) and Safety Data Sheets (SDS) are provided during technical scoping. Furthermore, we maintain third-party laboratory verification dossiers from accredited test centers covering ISO 10993 biocompatibility (in vitro cytotoxicity, skin sensitization, and intracutaneous irritation) to accelerate client 510(k) and CE MDR regulatory submissions.
What roll widths, core diameters, and packaging specifications can your slitting line accommodate?
Our German-engineered automated slitting and winding machines can produce roll widths from as narrow as 50 mm (for medical tape and bandage slit rolls) up to 3,200 mm for full-width surgical drapes. We accommodate standard internal paper or plastic core diameters of 76 mm (3 inches) and 152 mm (6 inches). Finished rolls undergo automated shrink-wrapping with heavy-gauge polyethylene film and desiccants, and can be palletized on fumigated wooden or plastic pallets with edge protectors to prevent transit crush damage during intermodal ocean transport.